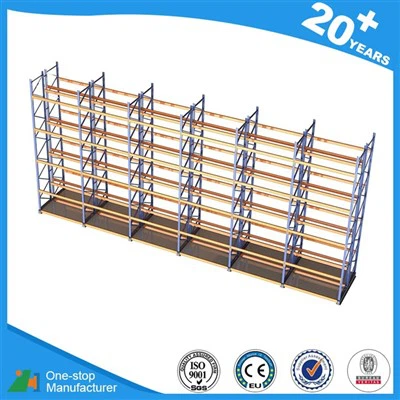


Nanjing Jinhui Storage Equipment Co., Ltd. is one of the leading manufacturers and suppliers of Motorized Mobile Racking System in China, also supports customized service. Welcome to buy advanced Motorized Mobile Racking System for sale here and get quotation from our factory. Quality products and reasonable price are available.
Products Description

JINHUI Motorized Mobile Racking System is a high-density warehouse storage solution that installs pallet racks on electrically driven mobile bases. Instead of keeping a fixed aisle between every rack row, the system opens only the aisle required for access, helping increase storage capacity while maintaining convenient pallet retrieval.
The system can be configured according to warehouse layout, pallet dimensions, load requirements, operating conditions and control requirements. It is suitable for industrial warehouses, distribution centers, cold storage and other projects where floor-space utilization is important.
Product Specifications
| Item | Specification |
|---|---|
| Product Name | Motorized Mobile Racking System |
| Category | Mobile Racking |
| Material | Q235 Steel |
| Drive Type | Motorized Mobile Base |
| Surface Treatment | Powder Coating |
| Color | Customized |
| Rack Dimensions | Customized |
| Load Capacity | Customized According to Project Requirements |
| Control Options | Automatic Linkage / PC Control / Remote Control |
| Power Supply | 220V / 380V |
| OEM & ODM | Available |
Mobile Base Technical Parameters
| Model | Load Capacity | Movement Speed | Motor Power | Power Supply Form | Power Supply | Control Mode | Safety Device |
|---|---|---|---|---|---|---|---|
| Railed | 32 tons/set | Max. 10 m/min | Max. 1.5 kW | Tow Cable / Synchronous Line | 220V / 380V | Automatic Linkage / PC Control / Remote Control | Channel Self-Locking / Automatic Detection / Emergency Stop / Sound and Light Alarm / Overload Protection / Overcurrent Protection |
| Trackless | 16 tons/set | Max. 10 m/min | Max. 1.5 kW | Tow Cable / Synchronous Line | 220V / 380V | Automatic Linkage / PC Control / Remote Control | Channel Self-Locking / Automatic Detection / Emergency Stop / Sound and Light Alarm / Overload Protection / Overcurrent Protection |
Final system configuration should be confirmed according to warehouse layout, rack size, load requirements and operating conditions.
Why Choose Motorized Mobile Racking?
High Storage Density
Reduces the number of permanent forklift aisles and allows more pallet positions within the same warehouse footprint.
01
Direct Pallet Access
The required aisle can be opened when needed, allowing forklifts to access specific pallet locations.
02
Motorized Operation
The rack rows move automatically through electrically driven mobile bases.
03
Flexible Configuration
Railed and trackless systems are available for different load capacities, floor conditions and warehouse layouts.
04
Safety-Oriented Design
Multiple detection, emergency stop and electrical protection functions can be integrated into the system.
05
How the Motorized Mobile Racking System Works
The pallet racks are installed on electrically powered mobile bases.
When an operator selects a storage location, the required rack rows move automatically along the floor-mounted rail or mobile path to open an access aisle.
The operating sequence is:
Select Location → Rack Rows Move → Required Aisle Opens → Forklift Accesses Goods → System Returns or Opens the Next Aisle
Only the aisle currently required for operation needs to remain open, allowing more warehouse floor area to be used for storage.
Main System Components
A typical motorized mobile racking system may include:
- Pallet rack frames
- Rack beams
- Mobile bases
- Electric motors
- Drive wheels
- Floor rails
- Control cabinet
- Electrical wiring
- Sensors
- Emergency stop devices
- Warning lights
- Safety detection devices
The specific configuration depends on the selected mobile system and project requirements.
Control Options
Motorized mobile racking can be configured with different control methods.
Automatic Linkage
Multiple rack rows can operate in coordination according to the selected aisle position.
PC Control
The system can be connected to computer-based control for centralized warehouse operation.
Remote Control
Operators can control rack movement remotely within the permitted operating area.
More advanced warehouse control functions can also be evaluated according to individual project requirements.
Typical Applications
-
Industrial Warehouses
Suitable for factories storing raw materials, components, work-in-process inventory and finished goods.
-
Distribution Centers
Helps increase pallet storage capacity while maintaining flexible access to inventory.
-
Cold Storage
Mobile racking is especially useful where refrigerated space is expensive and storage density is important.
-
High-Value Inventory Storage
Controlled aisle access and organized pallet locations can support warehouses storing high-value or controlled inventory.
-
Special Storage Environments
The system can also be considered for projects with specific space, access or operational requirements.

Mobile Racking for Cold Storage

Cold storage is one of the common applications for high-density mobile pallet racking.
Because refrigerated warehouse space has a relatively high construction and operating cost, reducing unnecessary aisles can help improve the utilization of available storage space.
For cold-storage projects, the design should consider:
- Operating temperature
- Electrical component suitability
- Motor and cable configuration
- Moisture and condensation
- Surface treatment
- Pallet load
- Forklift operation
The final system should be configured according to the actual cold-room environment.
Warehouse Layout Design
A motorized mobile racking system should be designed according to the complete warehouse layout rather than only the rack dimensions.
Important factors include:
- Warehouse length and width
- Clear height
- Column positions
- Doors and loading areas
- Fire protection systems
- Forklift aisle requirements
- Pallet dimensions
- Maximum load
- Required pallet positions
- Rack height
- Operating workflow
A detailed layout helps determine the number of mobile rack rows, aisle position and overall storage capacity.
What Information Is Needed for a Quotation?
To prepare a suitable layout and quotation, please provide:
- Warehouse dimensions
- Clear warehouse height
- Pallet length, width and height
- Maximum pallet weight
- Required storage quantity
- Number of SKUs
- Forklift model
- Forklift lifting height
- Warehouse floor condition
- Operating temperature
- Existing CAD drawing, if available
With this information, our team can evaluate the rack layout, load capacity and mobile system configuration.
Request a Customized Mobile Racking Solution
Send us your warehouse layout, pallet specifications, load requirements and target storage capacity.
Our team can help evaluate a suitable motorized mobile racking configuration for your project.
E-mail: export@jhrack.com
WhatsApp: +86 185 0252 7163
Hot Tags: Motorized Mobile Racking System, China, manufacturers, suppliers, factory, warehouse, customized, buy, price, quotation, for sale, Automatic Electric Mobile Pallet Storage Racking System, Heavy Duty Mobile Pallet Storage Racking System