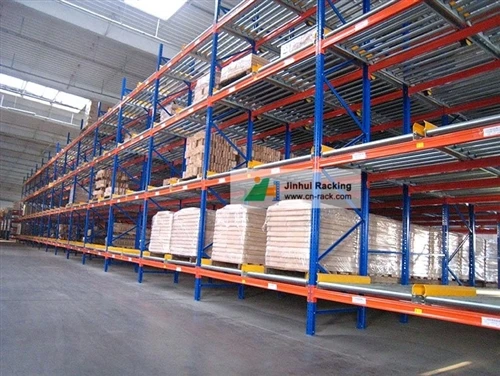

Shuttle racking, also known as carton flow racking or dynamic racking, is an advanced automated storage and retrieval system (AS/RS) designed to optimize warehouse space utilization and improve operational efficiency. Unlike traditional static racking systems, shuttle racking uses motorized shuttle carriers that move along rails installed within the rack structure, enabling the automatic transport of pallets between storage locations and loading/unloading points. This system operates on the FIFO (First-In-First-Out) or LIFO (Last-In-First-Out) principle, making it ideal for industries with high storage density needs, such as food and beverage, pharmaceuticals, cold storage, e-commerce, and retail logistics. By reducing manual handling, minimizing human error, and doubling storage capacity compared to conventional racking, shuttle racking has become a critical solution for modern warehouses seeking to streamline their supply chain operations. As the global demand for efficient storage systems continues to rise, Chinese manufacturers have emerged as key players in this sector, combining advanced technology, competitive pricing, and reliable after-sales service to serve both domestic and international markets.
1. Nanjing Jinhui Storage Equipment Co., Ltd.
Website: https://www.cn-rack.com/
Nanjing Jinhui Storage Equipment Co., Ltd. is a renowned specialist in the design, manufacturing, and installation of intelligent storage systems, with a strong focus on shuttle racking technology. Founded in 1998, the company has grown from a small local racking supplier to a leading industrial storage solution provider with over 25 years of experience in the field. Located in Nanjing, a major industrial hub in eastern China, Jinhui operates a modern production facility spanning 30,000 square meters, equipped with state-of-the-art manufacturing equipment including CNC punching machines, automatic welding lines, and precision powder coating systems. The company employs a team of over 200 professionals, including 30 experienced R&D engineers, 50 skilled production workers, and 40 dedicated after-sales service staff, ensuring that every aspect of their operations meets international quality standards.
Jinhui's shuttle racking products are designed to cater to a wide range of industry needs, from small warehouses to large-scale distribution centers. Their core shuttle racking series includes semi-automated and fully automated systems, with shuttle carriers capable of handling loads from 500kg to 2,500kg per pallet. The company's R&D team has developed innovative features such as anti-collision technology, intelligent load balancing, and wireless communication systems that enable seamless integration with warehouse management systems (WMS) and enterprise resource planning (ERP) software. This level of connectivity allows customers to monitor and control shuttle racking operations in real time, optimizing inventory management and reducing operational downtime.
In terms of quality assurance, Jinhui has implemented a strict quality control system that adheres to international standards such as ISO 9001, FEM (European Materials Handling Federation), and AS (Australian Standard). All raw materials used in their shuttle racking production, including high-quality steel from reputable Chinese mills, undergo rigorous testing for strength, durability, and corrosion resistance. The company's shuttle carriers are tested under extreme conditions to ensure reliability, with a minimum lifespan of 10 years even in high-volume operation environments. Jinhui also offers customized shuttle racking solutions, working closely with clients to assess their specific storage requirements, warehouse layout, and operational workflows to design tailored systems that maximize space utilization and efficiency.
The company has built a strong reputation for customer service, providing end-to-end support from initial consultation, design, and installation to ongoing maintenance and technical support. Their after-sales team offers 24/7 emergency service, with spare parts available globally through their extensive distribution network. Jinhui's shuttle racking systems have been successfully implemented in over 30 countries, including the United States, Germany, Australia, Japan, and Southeast Asian nations, serving clients in industries such as cold storage, food and beverage, pharmaceuticals, and e-commerce. Their commitment to innovation, quality, and customer satisfaction has earned them numerous awards, including the "China Storage Industry Top 10 Brand" in 2021 and 2022, further solidifying their position as a leading shuttle racking factory in China.
Nanjing Jinhui Storage Equipment Co., Ltd. Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Semi/full-automated shuttle carriers with 500-2500kg load capacity | Versatile for small to large warehouse needs, suitable for various pallet sizes || Intelligent WMS/ERP integration | Real-time monitoring, optimized inventory management, reduced manual errors || Anti-collision and load balancing technology | Enhanced safety, minimized downtime, increased operational reliability || ISO 9001, FEM, AS certified quality standards | Guaranteed product durability, compliance with international safety regulations || Customized design service | Tailored to specific warehouse layouts and operational workflows, maximum space utilization || 24/7 global after-sales support | Emergency service, quick spare parts delivery, long-term equipment maintenance || Corrosion-resistant powder coating | Suitable for cold storage and humid environments, extended product lifespan || High-density storage (up to 60% more than conventional racking) | Reduced warehouse footprint, lower operational costs |
2. Jiangsu Union Logistics System Engineering Co., Ltd.
Jiangsu Union Logistics System Engineering Co., Ltd. is a leading national high-tech enterprise specializing in intelligent logistics equipment and storage solutions, with a prominent focus on shuttle racking systems. Established in 2000, the company has its headquarters in Suzhou, Jiangsu, and operates three production bases with a total area of over 80,000 square meters, making it one of the largest shuttle racking manufacturers in eastern China. Union Logistics employs a team of more than 500 staff, including 120 technical professionals, 80 production engineers, and a dedicated international sales team, supported by a network of 15 regional offices across China and 5 overseas branches.
Union Logistics' shuttle racking product line encompasses shuttle racking for deep lane storage, double-deep shuttle racking, and automated shuttle racking systems integrated with robotic technology. Their shuttle carriers are designed with advanced motor systems and battery technology, achieving a maximum operating speed of 120 meters per minute and a continuous operation time of over 8 hours on a single charge. The company has invested heavily in R&D, with a national-level technology center that has developed over 50 patents related to shuttle racking technology, including intelligent positioning systems and energy-saving shuttle control algorithms. These innovations have enabled Union Logistics to offer shuttle racking solutions that deliver higher efficiency and lower energy consumption compared to many competitors.
The company's shuttle racking systems are widely used in industries requiring high-density storage, such as cold chain logistics, automotive parts storage, and chemical warehouses. Union Logistics has extensive experience in designing shuttle racking for low-temperature environments down to -30°C, with specialized materials and insulation features that ensure reliable performance in extreme cold conditions. Their products undergo comprehensive testing in their in-house testing laboratory, including load capacity tests, fatigue tests, and environmental resistance tests, to meet international standards such as ISO 14001 and OHSAS 18001. In addition to manufacturing, Union Logistics provides turnkey solutions, including system design, installation, commissioning, and operator training, ensuring that clients can quickly and effectively adopt their new shuttle racking systems.
Union Logistics has a strong presence in the global market, with shuttle racking exports to over 40 countries, including Europe, North America, the Middle East, and Australia. The company has established long-term partnerships with major international logistics companies and has completed several large-scale projects, including a 20,000 pallet shuttle racking system for a leading European food distributor and an automated shuttle racking system for an American e-commerce giant. Their commitment to sustainability is also a key focus, with shuttle racking designs that reduce energy consumption by up to 30% and use recyclable materials, aligning with global environmental standards. This combination of technical innovation, industry expertise, and global service has made Jiangsu Union Logistics a trusted name in the shuttle racking sector.
Jiangsu Union Logistics Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| High-speed shuttle carriers (120m/min) with 8+ hour battery life | Increased operational efficiency, reduced charging downtime || Deep lane and low-temperature (-30°C) specialized designs | Suitable for cold chain, chemical, and deep storage applications || 50+ technology patents and R&D center | Innovative solutions, competitive technological edge || ISO 14001 and OHSAS 18001 certified | Environmental compliance, safe working conditions || Turnkey project solutions from design to training | One-stop service, quick system adoption || Global network with overseas branches | Local support in international markets, faster response times || Energy-saving design (30% less consumption) | Lower operational costs, environmental sustainability || Large-scale project experience | Capable of handling complex, high-volume warehouse requirements |
3. Guangzhou Suprepack Storage Equipment Co., Ltd.
Guangzhou Suprepack Storage Equipment Co., Ltd. is a professional manufacturer and supplier of intelligent storage solutions, specializing in shuttle racking systems for the Asian and global markets. Founded in 2005 in Guangzhou, Guangdong Province, a major manufacturing and logistics hub in southern China, Suprepack has developed a strong reputation for delivering high-quality, cost-effective shuttle racking solutions. The company operates a 25,000 square meter production facility equipped with automated production lines, including laser cutting machines, robotic welding arms, and electrostatic powder coating equipment, ensuring precise and consistent product quality. Suprepack employs over 180 staff, including 25 R&D engineers, 60 production workers, and 35 international sales specialists, with a focus on serving small and medium-sized enterprises (SMEs) as well as large corporations.
Suprepack's shuttle racking product range includes standard shuttle racking, double shuttle racking, and customized shuttle systems tailored to specific client needs. Their shuttle carriers are designed with user-friendly control systems, featuring LCD touch screens for easy operation and compatibility with various pallet types, including euro pallets, industrial pallets, and custom-sized pallets. The company's R&D team has developed lightweight yet durable shuttle carriers that reduce overall system weight while maintaining high load capacity, resulting in lower installation costs and improved energy efficiency. Suprepack's shuttle racking systems support both FIFO and LIFO operations, making them flexible for different inventory management strategies.
Quality control is a core value at Suprepack, with every stage of production subject to strict inspection. Raw steel materials are sourced from leading Chinese suppliers such as Baosteel, and undergo testing for tensile strength and hardness before entering production. All shuttle racking components are coated with a durable powder finish that resists scratches, corrosion, and fading, even in high-humidity environments common in southern China. The company's products have earned certifications including ISO 9001:2015, CE, and SGS, ensuring compliance with international safety and quality standards. Suprepack also offers flexible pricing options and short delivery times, with standard shuttle racking systems available for delivery within 15 working days, a key advantage for time-sensitive projects.
In terms of customer service, Suprepack provides comprehensive support, including free on-site surveys, 3D design rendering, and installation guidance. The company's after-sales team offers 12-month warranty for all shuttle racking products, with affordable spare parts available globally. Suprepack has successfully completed over 2,000 projects in 30 countries, including Singapore, Malaysia, Indonesia, the United States, and Canada, serving industries such as food and beverage, electronics, pharmaceuticals, and retail. Their commitment to affordability, quality, and timely delivery has made them a popular choice among international clients seeking reliable shuttle racking solutions from China.
Guangzhou Suprepack Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Lightweight, durable shuttle carriers with multi-pallet compatibility | Reduced installation costs, versatile for various pallet types || 15-day standard delivery for ready-made systems | Fast project completion, meets tight deadlines || ISO 9001, CE, SGS certified products | International quality and safety compliance || User-friendly LCD control system | Easy operation, minimal training required || 12-month warranty + affordable spare parts | Long-term value, low maintenance costs || Flexible pricing for SMEs and large corporations | Cost-effective solutions for all budget ranges || Corrosion-resistant powder coating | Suitable for high-humidity environments || FIFO/LIFO operational support | Flexible inventory management options |
4. Shanghai Baolun Intelligent Storage Equipment Co., Ltd.
Shanghai Baolun Intelligent Storage Equipment Co., Ltd. is a leading provider of intelligent storage and logistics systems, with a specialized focus on automated shuttle racking technology. Established in 2002 in Shanghai, China's financial and industrial center, Baolun has built a strong expertise in integrating automation and storage solutions for complex warehouse operations. The company's production base spans 40,000 square meters, equipped with advanced automated manufacturing equipment, including a fully automated powder coating line and robotic assembly systems, enabling high-volume production with consistent quality. Baolun employs a team of over 300 professionals, including 70 R&D specialists, 100 skilled production workers, and 50 project managers, supporting both domestic and international clients.
Baolun's shuttle racking systems are designed for high-volume, 24/7 operation, making them ideal for large distribution centers and e-commerce fulfillment centers. Their core product is the automated shuttle racking system (AS/RS) integrated with shuttle carriers, which can handle up to 1,200 pallets per hour, significantly improving throughput compared to conventional racking. The company's shuttle carriers feature intelligent navigation technology, using RFID and barcode scanning to accurately locate pallets within the rack structure, reducing errors and improving operational efficiency. Baolun also offers shuttle racking systems with multi-level configurations, allowing for maximum vertical space utilization in warehouses with limited floor area.
The R&D team at Baolun has developed innovative features such as predictive maintenance technology for shuttle carriers, which monitors component performance in real time and alerts operators to potential issues before they cause downtime. This technology reduces maintenance costs by up to 25% and extends the lifespan of the shuttle racking system. Baolun's shuttle racking products undergo strict testing, including load capacity tests under 150% of rated load, salt spray tests for corrosion resistance, and vibration tests to ensure durability during transportation and operation. The company holds certifications including ISO 9001, ISO 14001, and CE, and has been recognized as a "National High-Tech Enterprise" in China, reflecting their commitment to technological innovation.
Baolun's project experience includes large-scale shuttle racking systems for major clients such as China Post, JD.com, and Siemens, among others. The company provides end-to-end services, from initial consulting and system design to installation, commissioning, and ongoing maintenance. Their project management team ensures that each project is completed on time and within budget, with minimal disruption to client operations during installation. Baolun also offers customized software integration, enabling seamless communication between the shuttle racking system and clients' WMS, ERP, or order management systems. With a strong focus on automation and intelligent technology, Shanghai Baolun has established itself as a key player in the advanced shuttle racking market in China.
Shanghai Baolun Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| High-throughput automated system (1,200 pallets/hour) | Fast order fulfillment, suitable for high-volume e-commerce || Predictive maintenance technology | Reduced downtime, lower maintenance costs || Intelligent RFID/barcode navigation | Accurate pallet location, minimal human error || National High-Tech Enterprise certification | Advanced technology, innovative solutions || Multi-level vertical configuration | Maximizes space in warehouses with limited floor area || Seamless WMS/ERP software integration | Unified warehouse operations, improved efficiency || Strict 150% load testing | Guaranteed structural safety and durability || Large client project experience | Proven track record with major international and domestic brands |
5. Qingdao Ever Storage Equipment Co., Ltd.
Qingdao Ever Storage Equipment Co., Ltd. is a professional manufacturer of shuttle racking and other industrial storage systems, located in Qingdao, a major port city in Shandong Province, China. Founded in 2008, the company has grown rapidly to become a leading shuttle racking exporter, leveraging its proximity to Qingdao Port for efficient international shipping. Ever Storage operates a 35,000 square meter production facility, equipped with advanced manufacturing equipment including CNC turret punch presses, automatic brake presses, and a full automated powder coating line. The company employs over 220 staff, including 30 R&D engineers, 70 production workers, and 40 international sales specialists, with a focus on delivering cost-effective shuttle racking solutions to global clients.
Ever Storage's shuttle racking product line includes standard shuttle racking, double-deep shuttle racking, and custom-designed shuttle systems for specific industries. Their shuttle carriers are designed with a compact structure, allowing them to operate in narrow aisles, maximizing space utilization in warehouses. The company offers shuttle racking systems with load capacities ranging from 800kg to 3,000kg per pallet, suitable for a wide range of goods from small cartons to heavy industrial products. Ever Storage's R&D team has developed energy-efficient shuttle control systems that reduce power consumption by up to 20% compared to traditional models, helping clients lower operational costs.
Quality control is a priority at Ever Storage, with every component of their shuttle racking systems undergoing rigorous testing. Raw steel is sourced from reputable Chinese mills, and each rack beam is tested for bending strength to ensure it meets or exceeds international standards. The company's shuttle carriers are tested for durability over 10,000 operating cycles, ensuring reliable performance for years. Ever Storage's shuttle racking products have earned certifications including ISO 9001, CE, and SGS, and are exported to over 35 countries, including the United States, Germany, the United Kingdom, Australia, and Brazil. The company offers flexible customization services, working closely with clients to design shuttle racking solutions that fit their specific warehouse layout and operational needs.
In terms of customer support, Ever Storage provides free technical consultation, 3D design drawings, and installation guidance. The company offers a 10-year warranty for rack structures and a 2-year warranty for shuttle carriers, demonstrating confidence in their product quality. Their after-sales team provides timely technical support, with spare parts available for delivery within 7 working days globally. Ever Storage has completed numerous successful projects in various industries, including food and beverage, automotive, and manufacturing, earning a reputation for reliable products and competitive pricing. Their strategic location in Qingdao, with easy access to international shipping routes, makes them a preferred choice for global clients looking for shuttle racking manufacturers in China.
Qingdao Ever Storage Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Compact shuttle carriers for narrow aisles | Maximizes warehouse space utilization || 800-3000kg load capacity range | Versatile for various goods and industries || 20% energy-efficient control systems | Lower operational costs, environmental savings || 10-year rack structure warranty + 2-year shuttle warranty | Long-term product reliability, peace of mind || Proximity to Qingdao Port | Efficient international shipping, reduced delivery times || ISO 9001, CE, SGS certification | International quality and safety compliance || Flexible customization service | Tailored to specific warehouse layouts || Quick spare parts delivery (7 working days) | Minimizes downtime for clients |
6. Tianjin Xinhua Rigid Storage Co., Ltd.
Tianjin Xinhua Rigid Storage Co., Ltd. is a leading manufacturer of intelligent shuttle racking systems and industrial storage solutions, based in Tianjin, a major industrial and logistics hub in northern China. Founded in 1995, the company has over 28 years of experience in the storage equipment industry, specializing in heavy-duty shuttle racking for demanding industrial applications. Xinhua Rigid operates two production bases with a total area of 60,000 square meters, equipped with advanced manufacturing technology including automated welding lines, robotic coating systems, and precision testing equipment. The company employs over 400 staff, including 85 technical professionals, 150 production workers, and 60 project management specialists, supporting domestic and international clients across various industries.
Xinhua Rigid's shuttle racking systems are designed for heavy-load applications, with a focus on durability and reliability in challenging environments. Their heavy-duty shuttle carriers can handle loads up to 3,500kg per pallet, making them ideal for storing large, heavy goods such as automotive parts, construction materials, and industrial machinery components. The company's shuttle racking structures are engineered with high-tensile steel, ensuring they can withstand heavy loads and frequent operation without deformation. Xinhua Rigid has developed specialized shuttle racking for high-temperature environments up to 60°C, suitable for warehouses storing heat-sensitive industrial products or operating in hot climates.
The R&D team at Xinhua Rigid has developed innovative shuttle navigation technology that ensures precise movement even in long rack lanes, reducing the risk of pallet damage and system errors. Their shuttle carriers feature anti-slip wheels and shock-absorption systems, enhancing safety during operation. All shuttle racking products undergo comprehensive load testing, including static load tests, dynamic load tests, and fatigue tests, to meet international standards such as FEM and ISO. Xinhua Rigid holds certifications including ISO 9001, ISO 14001, and OHSAS 18001, and has been recognized as a "Tianjin Famous Brand" for their high-quality storage equipment.
Xinhua Rigid has extensive project experience, having completed over 5,000 shuttle racking projects in 40 countries, including Russia, Germany, the United States, and Australia. The company provides turnkey solutions, from design and manufacturing to installation and after-sales service, with a team of experienced engineers who ensure that each project is tailored to client needs. Their after-sales support includes regular maintenance checks, technical training for operators, and 24/7 emergency service. Xinhua Rigid's commitment to heavy-duty design, technical innovation, and customer satisfaction has made them a trusted name in the shuttle racking industry, particularly for clients with demanding industrial storage requirements.
Tianjin Xinhua Rigid Storage Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Heavy-duty carriers (up to 3,500kg load capacity) | Suitable for large, heavy industrial goods || High-temperature resistant design (up to 60°C) | Operates effectively in hot environments || Anti-slip wheels and shock-absorption systems | Enhanced safety, reduced pallet damage || FEM and ISO certified load testing | Guaranteed structural safety and durability || Turnkey project solutions | End-to-end support for complex projects || Tianjin Famous Brand recognition | Established brand reputation in northern China || 24/7 emergency after-sales service | Quick response to technical issues || 5,000+ global project experience | Proven track record in heavy-duty applications |
7. Hangzhou Yiwei Intelligent Technology Co., Ltd.
Hangzhou Yiwei Intelligent Technology Co., Ltd. is a specialized intelligent storage system manufacturer focusing on automated shuttle racking and robotics-integrated storage solutions. Founded in 2010 in Hangzhou, a city known for its technology and innovation in eastern China, Yiwei has rapidly emerged as a leader in the intelligent storage sector, particularly for e-commerce and retail logistics. The company operates a 20,000 square meter production and R&D center, equipped with cutting-edge technology including automated assembly lines and a smart testing laboratory. Yiwei employs over 150 staff, including 40 R&D engineers, 50 production workers, and 30 international sales specialists, with a strong focus on innovation and smart warehouse solutions.
Yiwei's shuttle racking systems are designed for integration with robotic technology, creating hybrid automated storage and retrieval systems (AS/RS) that combine the benefits of shuttle racking with robotic picking. Their shuttle carriers are compatible with various robotic picking arms, enabling efficient pallet movement and order picking in e-commerce warehouses. The company's core shuttle racking product features modular design, allowing for easy expansion and reconfiguration as client needs change. Yiwei's R&D team has developed a cloud-based control system for shuttle racking, enabling remote monitoring and management of storage operations from any location, a key advantage for multi-location businesses.
Yiwei's shuttle racking systems are ideal for e-commerce and retail, supporting high-throughput order fulfillment and efficient inventory management. Their products support both FIFO and LIFO operations, with intelligent software that optimizes pallet placement to minimize picking time. The company's shuttle carriers are designed for fast operation, with a maximum speed of 150 meters per minute, reducing order processing time. All Yiwei shuttle racking products undergo rigorous testing for reliability, with a minimum 8-hour continuous operation time per charge and a battery lifespan of over 5 years. The company holds certifications including ISO 9001, CE, and China High-Tech Enterprise, reflecting their commitment to technological innovation.
Yiwei has completed numerous projects for leading e-commerce clients in China and abroad, including Alibaba, Pinduoduo, and various retail chains. The company provides customized solutions, including 3D virtual reality (VR) design to help clients visualize their shuttle racking system before installation. Yiwei's after-sales service includes operator training, remote technical support, and annual maintenance packages, ensuring long-term system performance. Their focus on intelligent technology and e-commerce-specific solutions has made Hangzhou Yiwei a key player in the modern shuttle racking market, catering to the growing needs of the digital logistics sector.
Hangzhou Yiwei Intelligent Technology Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Robotics-integrated hybrid AS/RS systems | Efficient order picking for e-commerce and retail || Cloud-based remote monitoring | Global access to system management, ideal for multi-location businesses || High-speed shuttle carriers (150m/min) | Fast order processing, reduced fulfillment time || Modular design | Easy system expansion and reconfiguration || VR design visualization | Clear pre-installation planning for clients || China High-Tech Enterprise certification | Advanced intelligent technology || 5+ year battery lifespan | Lower replacement costs, extended system life || E-commerce specialized solutions | Tailored for high-throughput order fulfillment |
8. Shenzhen Leader Storage Equipment Co., Ltd.
Shenzhen Leader Storage Equipment Co., Ltd. is a professional manufacturer of shuttle racking and intelligent storage systems, located in Shenzhen, China's technology and manufacturing hub in the south. Established in 2003, the company has grown to become a leading supplier of shuttle racking for the electronics and high-tech industries, leveraging Shenzhen's strong manufacturing and technology ecosystem. Leader Storage operates a 28,000 square meter production facility, equipped with advanced manufacturing equipment including laser cutting, robotic welding, and automated powder coating lines, ensuring high precision and consistent quality. The company employs over 200 staff, including 35 R&D engineers, 65 production workers, and 40 international sales specialists.
Leader Storage's shuttle racking systems are designed specifically for the electronics industry, with features that protect sensitive electronic goods from damage and static electricity. Their shuttle carriers and rack structures are made with anti-static materials, preventing electrostatic discharge (ESD) that can damage electronic components. The company's shuttle racking systems are also designed for precise temperature and humidity control, ideal for storing sensitive electronics that require stable environmental conditions. Leader Storage offers shuttle racking with customized dimensions to fit electronic parts of various sizes, from small semiconductors to large consumer electronics.
The R&D team at Leader Storage has developed intelligent shuttle racking with inventory tracking technology, using RFID tags to monitor each pallet's location, quantity, and expiration date. This technology is critical for the electronics industry, where inventory accuracy is essential. Their shuttle systems feature low-noise operation, suitable for cleanroom environments common in electronics manufacturing facilities. All Leader Storage shuttle racking products undergo strict testing for ESD protection, temperature resistance, and durability, meeting international standards for electronics storage. The company holds certifications including ISO 9001, ISO 14001, and ESD association certification, ensuring compliance with industry-specific requirements.
Leader Storage's clients include leading electronics manufacturers such as Huawei, Foxconn, and Samsung, as well as logistics companies serving the tech industry. The company provides specialized solutions for cleanrooms, temperature-controlled warehouses, and ESD-protected storage areas. Their project services include on-site environmental assessment, customized design, and compliance with industry-specific safety regulations. Leader Storage's after-sales team has expertise in handling high-tech storage systems, providing technical support tailored to the electronics industry's unique needs. Their focus on industry-specific design and quality has made Shenzhen Leader Storage a trusted shuttle racking manufacturer for the high-tech sector.
Shenzhen Leader Storage Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Anti-static (ESD-protected) design | Safeguards sensitive electronic components || Temperature/humidity controlled options | Ideal for storing temperature-sensitive electronics || RFID inventory tracking | High inventory accuracy, critical for tech industries || Low-noise operation | Suitable for cleanroom environments || Industry-specific ESD certification | Compliance with electronics storage standards || Customized dimensions for electronic parts | Versatile for various tech product sizes || Experience with major electronics brands | Proven track record in high-tech sectors || Specialized cleanroom solutions | Meets strict environment requirements |
9. Chongqing Shine Logistics Equipment Co., Ltd.
Chongqing Shine Logistics Equipment Co., Ltd. is a leading shuttle racking manufacturer in southwestern China, specializing in shuttle systems for cold storage and heavy-duty industrial applications. Founded in 2006 in Chongqing, a major logistics and manufacturing center in the Yangtze River basin, Shine Logistics has developed a strong reputation for reliable, cost-effective shuttle racking for challenging environments. The company operates a 32,000 square meter production facility, equipped with specialized equipment for producing cold-storage compatible storage systems, including low-temperature resistant steel and insulation materials. Shine Logistics employs over 180 staff, including 30 R&D engineers, 70 production workers, and 35 international sales specialists, with a focus on cold chain and industrial clients.
Shine Logistics' shuttle racking systems are specifically designed for cold storage facilities, with materials that can withstand temperatures as low as -40°C. Their shuttle carriers feature insulated components and specialized batteries that perform reliably in extreme cold, eliminating the need for frequent replacements or repairs due to low-temperature damage. The company's cold storage shuttle racking has a modular design that allows for easy installation in existing cold warehouses, minimizing downtime during setup. Shine Logistics also offers heavy-duty shuttle racking for general industrial use, with load capacities up to 3,200kg per pallet, suitable for heavy goods in manufacturing and distribution.
The R&D team at Shine Logistics has developed shuttle control systems optimized for cold environments, with enhanced heating for electronic components to prevent malfunction in low temperatures. Their cold storage shuttle racking systems also feature corrosion-resistant coatings, protecting against moisture and frost common in cold storage facilities. All products undergo testing in simulated low-temperature environments to ensure performance before delivery. Shine Logistics holds certifications including ISO 9001, ISO 14001, and HACCP, making their shuttle racking suitable for food cold storage applications that require food safety compliance.
Shine Logistics has extensive experience in cold storage shuttle racking projects, including installations for major food distributors and pharmaceutical cold chain companies in China and Southeast Asia. The company provides end-to-end support, including design, cold environment testing, installation, and maintenance tailored for low-temperature operations. Their after-sales team is trained to work in cold storage facilities, offering on-site support and spare parts designed for extreme temperatures. With a focus on cold storage expertise and competitive pricing, Chongqing Shine Logistics has become a leading shuttle racking manufacturer for the cold chain industry.
Chongqing Shine Logistics Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Low-temperature resistant (up to -40°C) | Suitable for deep-freeze cold storage facilities || Insulated shuttle components | Reliable performance in extreme cold, no electronic malfunction || HACCP certified | Compliance with food safety standards for cold storage || Heavy-duty design (up to 3,200kg load) | Versatile for cold and industrial applications || Modular design for easy installation | Minimal downtime in existing warehouses || Corrosion-resistant coating | Protection against frost and moisture || Cold chain specialized expertise | Deep understanding of low-temperature storage needs || Southeast Asia project experience | Local support for international cold chain clients |
10. Zhejiang Jiali Storage Technology Co., Ltd.
Zhejiang Jiali Storage Technology Co., Ltd. is a professional manufacturer and supplier of shuttle racking and intelligent storage systems, based in Zhejiang Province, a leading manufacturing and export hub in eastern China. Founded in 2001, Jiali has over 22 years of experience in the storage equipment industry, with a focus on medium-duty shuttle racking for small to medium-sized warehouses. The company operates a 25,000 square meter production facility, equipped with modern manufacturing lines including CNC cutting, automatic bending, and powder coating systems, ensuring efficient production and consistent quality. Jiali employs over 160 staff, including 25 R&D engineers, 55 production workers, and 30 international sales specialists, with a mission to provide affordable, reliable shuttle racking for businesses of all sizes.
Jiali's shuttle racking product line includes standard semi-automated shuttle systems, ideal for SMEs with limited budgets and moderate storage needs. Their shuttle carriers have a load capacity of 600kg to 1,800kg per pallet, suitable for light to medium goods such as food products, retail goods, and small industrial parts. The company's shuttle racking structures feature a lightweight yet durable design, reducing installation time and cost. Jiali offers both standard shuttle racking models and customized solutions, working closely with clients to adjust dimensions and features to fit their specific warehouse requirements.
The R&D team at Jiali has developed user-friendly shuttle control software, compatible with basic WMS systems or even manual operation for smaller businesses. Their shuttle systems are easy to operate, requiring minimal training for warehouse staff, a key advantage for SMEs with limited technical resources. All Jiali shuttle racking products undergo strict quality testing, including load tests, corrosion tests, and operation cycle tests, to ensure durability. The company holds certifications including ISO 9001, CE, and SGS, ensuring international quality and safety compliance. Jiali offers competitive pricing, with shuttle racking systems priced 10-15% lower than many premium brands, making them an attractive option for budget-conscious clients.
Jiali has completed over 1,500 projects in 25 countries, including European nations, Southeast Asia, and Africa, serving small businesses, local distributors, and medium-sized manufacturers. The company provides comprehensive support, including free design consultation, installation guidance, and a 10-year warranty for rack structures and a 1-year warranty for shuttle carriers. Their after-sales team offers technical support in multiple languages, ensuring accessibility for international clients. With a focus on affordability, ease of use, and reliability, Zhejiang Jiali Storage Technology has established itself as a leading shuttle racking manufacturer for SMEs and mid-market clients.
Zhejiang Jiali Storage Technology Shuttle Racking Features & Advantages
| Features | Advantages ||----------|------------|| Medium load capacity (600-1,800kg) | Suitable for light to medium goods, SMEs || User-friendly control software | Minimal training required for staff || Lightweight structure | Reduced installation time and cost || 10-year rack warranty + 1-year shuttle warranty | Long-term reliability for mid-range budgets || 10-15% lower pricing than premium brands | Cost-effective for budget-conscious clients || ISO 9001, CE, SGS certification | International quality compliance || Multi-language technical support | Accessible for international clients || SME-focused solutions | Tailored for small to medium warehouse needs |
Summary
China's shuttle racking manufacturing industry has emerged as a global leader, offering a diverse range of high-quality, innovative solutions to meet the evolving needs of warehouses across industries worldwide. The 10 leading factories profiled in this article represent the breadth of expertise in the Chinese market, from large-scale automated systems for e-commerce and heavy industrial applications to specialized solutions for cold storage, electronics, and small and medium-sized enterprises. Each manufacturer brings unique strengths to the table: Nanjing Jinhui stands out for its reliable quality and comprehensive global support, Jiangsu Union Logistics excels in high-speed, high-volume systems for cold chains, while Guangzhou Suprepack offers cost-effective solutions for SMEs. Shanghai Baolun and Hangzhou Yiwei lead in intelligent, robotics-integrated systems for modern digital logistics, while Qingdao Ever Storage and Tianjin Xinhua Rigid specialize in heavy-duty and port-friendly designs. Shenzhen Leader Storage caters to the high-tech sector's ESD and cleanroom needs, Chongqing Shine excels in low-temperature cold storage systems, and Zhejiang Jiali provides affordable, user-friendly solutions for mid-market clients. Together, these manufacturers demonstrate China's capability to combine advanced technology, competitive pricing, and customer-centric service to deliver shuttle racking systems that optimize warehouse efficiency, reduce operational costs, and support global supply chain growth. As the demand for automated storage continues to rise, these leading Chinese shuttle racking factories are well-positioned to drive innovation and serve the growing needs of the global logistics industry.