
Introduction to Pallet Racking
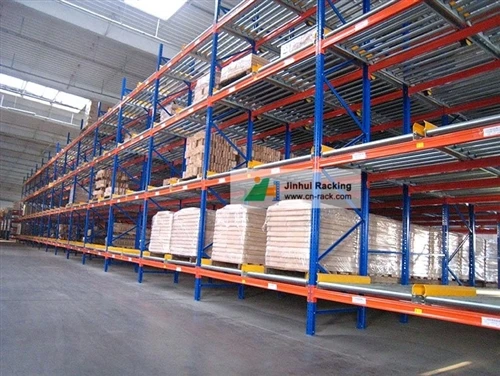
Pallet racking is a critical component of modern warehousing and logistics infrastructure, designed to store palletized goods in an organized, space-efficient manner. These systems enable businesses to maximize vertical storage capacity, improve inventory accessibility, streamline order picking processes, and enhance overall warehouse operational efficiency. Pallet racking systems come in various configurations, including selective rack, drive-in rack, double-deep rack, cantilever rack, and push-back rack, each tailored to specific storage needs, product types, and warehouse layouts. As global supply chains continue to evolve, the demand for high-quality, durable, and customized pallet racking solutions has grown exponentially, making the selection of a reliable supplier a key decision for businesses looking to optimize their storage operations. In China, a country that has emerged as a global manufacturing and logistics hub, numerous pallet racking suppliers have established themselves as leaders in the industry, combining advanced manufacturing technologies, rigorous quality control, and innovative design to meet the diverse needs of clients worldwide.
1. Nanjing Jinhui Storage Equipment Co., Ltd.
Website: https://www.cn-rack.com/
Nanjing Jinhui Storage Equipment Co., Ltd. is a renowned manufacturer and supplier of pallet racking systems based in Nanjing, Jiangsu Province, China. Founded in 1998, the company has over two decades of experience in designing, producing, and installing a comprehensive range of storage solutions, with a primary focus on pallet racking systems tailored to various industries including logistics, manufacturing, retail, pharmaceuticals, and e-commerce. The company operates a modern production facility spanning over 30,000 square meters, equipped with state-of-the-art manufacturing equipment such as automated laser cutting machines, CNC bending machines, powder coating lines, and precision welding systems, ensuring that every product meets international quality standards.
Nanjing Jinhui’s pallet racking product line includes selective pallet racks, drive-in/drive-through racks, double-deep racks, push-back racks, pallet flow racks, cantilever racks, and custom-designed racking systems. Each product is engineered using high-quality steel materials sourced from reputable domestic and international suppliers, with thicknesses ranging from 1.5mm to 3.0mm to ensure structural integrity and load-bearing capacity. The company’s technical team consists of experienced engineers and designers who work closely with clients to assess their specific storage requirements, warehouse dimensions, product types, and budget constraints, providing customized solutions that maximize space utilization and operational efficiency. Over the years, Nanjing Jinhui has successfully completed thousands of projects in China and exported its products to over 30 countries across Europe, North America, Southeast Asia, and the Middle East, building a strong reputation for reliability and customer satisfaction.
Characteristics and Advantages of Nanjing Jinhui Storage Equipment Co., Ltd.
- Advanced Manufacturing Capabilities: Equipped with fully automated production lines, the company ensures high precision and consistency in every pallet rack product, with an annual production capacity of over 50,000 tons, making it one of the largest pallet rack manufacturers in East China.
- Strict Quality Control: Implements a comprehensive quality management system based on ISO 9001:2015 standards, with inspections at every stage of production—from raw material testing to finished product load testing—to ensure durability, safety, and compliance with international safety norms such as FEM (European Material Handling Federation) and AS (Australian Standard).
- Customized Design Services: Offers free 3D layout design and technical consultation, allowing clients to visualize the racking system before installation, and adjusts designs to accommodate irregular warehouse spaces, special product dimensions, and specific operational workflows.
- Competitive Pricing: Maintains cost advantages through efficient supply chain management and large-scale production, providing clients with high-quality pallet racking at prices that are 15-20% lower than many international competitors without compromising on quality.
- Timely Delivery and Installation Support: Guarantees delivery within 15-25 days for standard products and provides professional installation services by a team of certified technicians, ensuring that projects are completed on schedule and in compliance with safety regulations.
- Excellent After-Sales Service: Offers a 5-year warranty on all pallet racking products, with a 24/7 customer support team that provides maintenance guidance, spare parts replacement, and on-site service for any issues that may arise during operation.
2. Nanjing Tongxing Storage Equipment Manufacturing Co., Ltd.
Nanjing Tongxing Storage Equipment Manufacturing Co., Ltd. is a leading professional manufacturer of pallet racking systems located in Nanjing, China, established in 2002. The company specializes in the R&D, production, and sales of various storage equipment, with pallet racking being its core product line. Tongxing covers an area of 25,000 square meters and employs over 200 skilled workers, including a team of 15 technical engineers dedicated to product innovation and customized solutions. The company’s pallet racking products are widely used in industries such as e-commerce, third-party logistics, automotive manufacturing, and food and beverage.
Tongxing’s pallet racking range includes selective pallet racks, double-deep pallet racks, drive-in racks, pallet flow racks, and heavy-duty cantilever racks. All products are made from high-quality Q235B steel, with surface treatments including hot-dip galvanizing and powder coating to enhance corrosion resistance and durability, making them suitable for both indoor and outdoor use. The company invests heavily in R&D, having developed several patented technologies for rack stability and load optimization, ensuring that its products can support heavy loads of up to 5,000 kg per beam. Tongxing has exported its pallet racking to more than 20 countries, including the United States, Germany, Australia, and Russia, and has established long-term partnerships with many global logistics enterprises.
Characteristics and Advantages of Nanjing Tongxing Storage Equipment Manufacturing Co., Ltd.
- Patented Technological Innovation: Holds 8 national patents related to pallet rack design, including a unique beam connector that improves load stability by 30% and reduces installation time by 25%.
- Specialized Industry Solutions: Offers tailored pallet racking solutions for specific industries, such as climate-controlled racks for pharmaceuticals, high-density racks for e-commerce order centers, and heavy-duty racks for automotive parts storage.
- Strict Compliance with International Standards: Products are certified by ISO 9001, ISO 14001, and TÜV, ensuring compliance with European and North American safety and environmental standards.
- Large Production Capacity: Annual production of pallet racking exceeds 40,000 tons, allowing the company to handle large-scale orders efficiently, even for projects requiring over 10,000 racking units.
- Customized Surface Treatments: Provides options for hot-dip galvanizing (for outdoor use) and electrostatic powder coating in various colors, meeting clients’ aesthetic and functional needs.
- Responsive Customer Support: Offers free on-site surveys for large projects, detailed technical drawings, and a 3-year warranty, with a spare parts supply network that ensures quick replacements within 7 days globally.
3. Jiangsu Union Racking Technology Co., Ltd.
Jiangsu Union Racking Technology Co., Ltd. is a high-tech enterprise specializing in the research, development, production, and sales of pallet racking systems, located in Suzhou, Jiangsu, a major manufacturing hub in China. Founded in 2005, the company has grown to become one of the most innovative pallet racking suppliers in the country, focusing on smart storage solutions that integrate pallet racking with automated systems. Union Racking operates a 40,000-square-meter production facility equipped with advanced automated production lines, including robotic welding systems and intelligent powder coating lines, ensuring high efficiency and product consistency.
The company’s pallet racking product line includes not only traditional systems such as selective racks, drive-in racks, and push-back racks but also smart pallet racking solutions integrated with IoT (Internet of Things) sensors, automated guided vehicles (AGVs), and warehouse management systems (WMS). These smart systems enable real-time inventory tracking, load monitoring, and automated picking, making Union Racking a preferred supplier for high-tech e-commerce and manufacturing enterprises. The company serves clients across over 25 countries, with key markets in Europe, North America, and Asia Pacific, and has completed projects for well-known brands such as Alibaba, JD.com, and Foxconn.
Characteristics and Advantages of Jiangsu Union Racking Technology Co., Ltd.
- Smart Pallet Racking Expertise: Pioneer in integrating IoT and automation into pallet racking, offering smart racking systems that provide real-time data on pallet location, load weight, and storage conditions, improving warehouse operational efficiency by up to 40%.
- High-Tech Production Equipment: Uses robotic welding and automated quality inspection systems, reducing human error and ensuring that 99.5% of products meet quality standards, with a production efficiency 30% higher than traditional manufacturers.
- Strong R&D Investment: Allocates 12% of annual revenue to R&D, with a dedicated team of 30 engineers working on new racking technologies, resulting in 15 patents for smart storage solutions.
- Comprehensive Product Range: Offers both standard and customized pallet racking, including specialized racks for fragile goods, hazardous materials, and cold storage environments.
- Integration with Automated Systems: Provides end-to-end solutions, including racking design, AGV compatibility testing, WMS integration, and on-site installation of automated systems.
- Global Certification and Support: Products are certified by TÜV, SGS, and ISO, and the company has local service teams in 8 countries, providing 24/7 technical support and maintenance.
4. Guangdong Dexion Storage Equipment Co., Ltd.
Guangdong Dexion Storage Equipment Co., Ltd. is a leading pallet racking supplier based in Guangzhou, Guangdong, with a history dating back to 1992. The company is a joint venture between Dexion Group, a global leader in storage solutions, and Chinese investors, combining international expertise with local manufacturing capabilities. Guangdong Dexion specializes in the production of high-quality pallet racking systems for industries including logistics, retail, manufacturing, and pharmaceuticals. The company operates a modern production facility spanning 50,000 square meters, with a focus on precision engineering and strict quality control.
Guangdong Dexion’s pallet racking products are known for their durability and versatility, including selective pallet racks, double-deep racks, drive-in racks, pallet flow racks, and cantilever racks. The company uses premium steel materials and advanced powder coating technology, ensuring that its racks can support heavy loads while resisting corrosion and wear. Over the years, Guangdong Dexion has established a strong presence in both domestic and international markets, exporting to over 30 countries and serving many Fortune 500 companies. The company is also committed to sustainable manufacturing, using eco-friendly materials and energy-efficient production processes.
Characteristics and Advantages of Guangdong Dexion Storage Equipment Co., Ltd.
- International Brand Partnership: Joint venture with Dexion Group, providing access to global design standards and technical expertise, ensuring that products meet the highest international quality requirements.
- Durable and Load-Bearing Design: Pallet racks are engineered with a unique beam-locking system that improves load stability, with some models supporting up to 6,000 kg per beam, making them suitable for heavy industrial applications.
- Eco-Friendly Manufacturing: Uses water-based powder coating processes that reduce VOC (volatile organic compound) emissions by 40% compared to traditional solvent-based coatings, aligning with global environmental standards.
- Extensive Product Testing: Conducts rigorous load testing and stress tests on all pallet racking products in its in-house testing laboratory, ensuring safety and reliability for long-term use.
- Global Distribution Network: Has a distribution network in 12 countries, enabling fast delivery to international clients, with standard products available for shipment within 10 days.
- Customized Safety Solutions: Offers additional safety features such as rack protectors, guardrails, and fire-resistant coatings, enhancing the safety of warehouse operations.
5. Zhejiang Hualong Storage Equipment Co., Ltd.
Zhejiang Hualong Storage Equipment Co., Ltd. is a professional manufacturer of pallet racking systems located in Hangzhou, Zhejiang, established in 1995. The company specializes in the design, production, and installation of various storage solutions, with pallet racking being its core business. Hualong covers an area of 35,000 square meters and employs over 250 people, including a team of 20 technical engineers and designers. The company’s pallet racking products are widely used in industries such as e-commerce, logistics, automotive, and electronics, and are exported to more than 20 countries worldwide.
Hualong’s pallet racking product line includes selective pallet racks, drive-in racks, push-back racks, pallet flow racks, and heavy-duty cantilever racks. All products are made from high-quality Q235B and Q355B steel, with surface treatments including electrostatic powder coating and hot-dip galvanizing to ensure corrosion resistance. The company invests in advanced production equipment, including CNC punching machines, bending machines, and automatic welding lines, to ensure product precision and quality. Hualong has a strong focus on customer service, providing customized solutions, free design services, and timely after-sales support to clients.
Characteristics and Advantages of Zhejiang Hualong Storage Equipment Co., Ltd.
- Cost-Effective Standard Products: Offers a wide range of standard pallet racking models with competitive prices, making it a popular choice for small and medium-sized enterprises (SMEs) looking for affordable storage solutions.
- Precision Production Technology: Uses CNC machining for all rack components, ensuring a tight fit between parts and reducing installation time by up to 20% compared to manually fabricated racks.
- Specialized Racks for Electronics Industry: Develops anti-static pallet racking systems suitable for electronic component storage, with features that prevent static electricity damage and meet industry-specific requirements.
- Flexible Order Quantities: Accepts small-volume orders (as low as 10 racking units) for custom projects, catering to the needs of businesses with limited storage space or budget.
- Local and Global Service Network: Has installation teams in major Chinese cities and agents in 8 international countries, providing on-site support for projects across Asia, Europe, and Africa.
- Long-Term Warranty: Provides a 5-year warranty on all standard pallet racking products, with optional extended warranty plans for customized and heavy-duty systems.
6. Shanghai NOTEK Storage Equipment Co., Ltd.
Shanghai NOTEK Storage Equipment Co., Ltd. is a leading provider of pallet racking and intelligent storage solutions based in Shanghai, China, founded in 2000. The company focuses on the R&D, production, and sales of high-end pallet racking systems, serving industries such as aviation, pharmaceuticals, high-tech manufacturing, and large-scale logistics. NOTEK operates a 45,000-square-meter production facility equipped with advanced automation equipment, including robotic welding systems and intelligent powder coating lines, ensuring the highest quality and efficiency.
NOTEK’s pallet racking product range includes selective pallet racks, double-deep racks, drive-in racks, pallet flow racks, and automated pallet racking systems integrated with AGVs and WMS. The company’s products are designed to meet strict international standards, with certifications from ISO 9001, TÜV, and SGS. Over the years, NOTEK has completed numerous high-profile projects, including pallet racking systems for Shanghai Pudong International Airport’s logistics center and leading pharmaceutical enterprises such as Sinopharm. The company is committed to innovation, investing a significant portion of its revenue in R&D to develop new and improved pallet racking solutions.
Characteristics and Advantages of Shanghai NOTEK Storage Equipment Co., Ltd.
- High-End Product Quality: Uses premium grade Q355B steel for heavy-duty pallet racks, with a yield strength 20% higher than standard Q235B steel, making products suitable for extreme load conditions.
- Automated Storage Solutions: Specializes in designing and installing automated pallet racking systems that work with AGVs, shuttle cars, and WMS, enabling fully automated storage and retrieval operations, reducing labor costs by up to 50%.
- Compliance with Aviation and Pharmaceutical Standards: Meets strict industry-specific standards, including ATA (Air Transport Association) standards for aviation logistics and GMP (Good Manufacturing Practices) for pharmaceutical storage, ensuring product safety and quality.
- In-House Testing Laboratory: Operates a state-of-the-art testing lab where all pallet racking products undergo load capacity, stability, and corrosion resistance tests, ensuring they meet or exceed international safety standards.
- Project Management Excellence: Assigns dedicated project managers to each client, overseeing the entire process from design and production to installation and training, ensuring projects are completed on time and to specifications.
- Global Client Base: Exports pallet racking to over 25 countries, with a focus on high-value markets in North America, Europe, and Oceania, and has established partnerships with multinational corporations.
7. Shandong Heavy Industry Storage Equipment Co., Ltd.
Shandong Heavy Industry Storage Equipment Co., Ltd. is a subsidiary of the Shandong Heavy Industry Group, a leading Chinese manufacturing conglomerate, located in Jinan, Shandong. Established in 2003, the company leverages the group’s strong manufacturing capabilities and technical expertise to produce high-quality pallet racking systems for industrial and logistics applications. The company operates a 60,000-square-meter production facility, making it one of the largest pallet rack manufacturers in northern China.
Shandong Heavy Industry’s pallet racking product line includes selective pallet racks, drive-in racks, double-deep racks, push-back racks, and heavy-duty cantilever racks, with a focus on heavy industrial applications such as automotive manufacturing, steel storage, and large-scale logistics. The company uses advanced production technology, including robotic welding and automated powder coating, to ensure product quality and consistency. With the support of its parent group, the company has strong financial resources and technical capabilities, allowing it to handle large-scale, complex projects. Shandong Heavy Industry’s pallet racking products are exported to over 15 countries and used by many well-known industrial enterprises in China.
Characteristics and Advantages of Shandong Heavy Industry Storage Equipment Co., Ltd.
- Heavy-Duty Industrial Expertise: Specializes in pallet racking for heavy industrial applications, with products supporting loads up to 8,000 kg per beam, making them ideal for storing large, heavy items such as automotive parts, steel coils, and heavy machinery components.
- Strong Manufacturing Backing: Part of Shandong Heavy Industry Group, which has over 70 years of manufacturing experience, providing access to advanced production technologies and quality control systems.
- Large-Scale Project Capability: Can complete projects requiring over 100,000 racking units, with an annual production capacity of over 60,000 tons, making it suitable for national-level logistics and industrial projects.
- Robust Quality Control: Implements strict quality management, with every pallet rack component tested for strength and durability, and products certified by ISO 9001 and TÜV.
- Competitive Pricing for Heavy-Duty Systems: Offers high-capacity pallet racking at prices lower than international competitors, due to integrated supply chain and manufacturing capabilities.
- National Service Network: Has installation and maintenance teams in all major Chinese industrial regions, providing fast support for large-scale projects across the country.
8. Fujian Anquan Storage Equipment Co., Ltd.
Fujian Anquan Storage Equipment Co., Ltd. is a professional pallet racking manufacturer located in Fuzhou, Fujian, established in 1999. The company specializes in the design, production, and installation of various storage solutions, with pallet racking as its core product. Anquan covers an area of 28,000 square meters and employs over 180 people, including a team of 12 technical engineers. The company’s pallet racking products are widely used in industries such as retail, e-commerce, food and beverage, and logistics, and are exported to over 15 countries in Southeast Asia, Europe, and the Middle East.
Anquan’s pallet racking product line includes selective pallet racks, drive-in racks, push-back racks, and cantilever racks, with a focus on safety and reliability. The company uses high-quality steel and advanced surface treatment technology to ensure that its racks are durable and resistant to corrosion, even in harsh environments. Anquan is committed to providing customized solutions to meet the unique needs of each client, working closely with customers to design racking systems that maximize storage space and improve operational efficiency. The company has built a strong reputation for its high-quality products and excellent customer service over the years.
Characteristics and Advantages of Fujian Anquan Storage Equipment Co., Ltd.
- Safety-Focused Design: All pallet racking products are designed with safety as a priority, incorporating features such as anti-collision guards, level indicators, and load limit markers to prevent accidents in warehouses.
- Affordable Customization: Offers cost-effective customized pallet racking solutions for small and medium-sized businesses, with flexible design options and short lead times of 10-15 days for standard custom projects.
- Corrosion Resistance: Provides multiple surface treatment options, including powder coating, hot-dip galvanizing, and galvanized powder coating, making products suitable for use in humid coastal environments (common in Fujian) and outdoor settings.
- Strong Local Market Presence: Is one of the top pallet racking suppliers in Fujian, with a client base of over 500 domestic enterprises, including many well-known retail chains and logistics companies.
- Efficient Installation Service: Has a team of experienced installers who can complete projects of all sizes, from small retail warehouses to large logistics centers, with minimal disruption to client operations.
- Customer-Centric Service: Offers free design consultations, on-site surveys, and a 3-year warranty on all products, with a responsive customer support team available to address any issues.
9. Henan Ruijing Storage Equipment Co., Ltd.
Henan Ruijing Storage Equipment Co., Ltd. is a leading pallet racking manufacturer based in Zhengzhou, Henan, founded in 2001. The company specializes in the production of high-quality pallet racking systems, including selective racks, drive-in racks, double-deep racks, and pallet flow racks, serving industries such as manufacturing, logistics, e-commerce, and agriculture. Ruijing operates a 32,000-square-meter production facility equipped with advanced production equipment, including CNC cutting machines, automatic welding lines, and powder coating systems, ensuring product precision and quality.
Ruijing’s pallet racking products are made from high-quality Q235B and Q355B steel, with surface treatments that provide excellent corrosion resistance. The company has a strong focus on R&D, continuously improving its product designs to enhance load capacity and stability. Over the years, Ruijing has completed thousands of projects in China and exported its products to over 12 countries, including Russia, Kazakhstan, and Vietnam. The company is committed to providing clients with reliable, cost-effective pallet racking solutions and excellent after-sales service.
Characteristics and Advantages of Henan Ruijing Storage Equipment Co., Ltd.
- Agricultural Storage Specialization: Offers specialized pallet racking solutions for the agricultural industry, including racks for grain storage, fertilizer storage, and agricultural product warehouses, designed to withstand heavy loads and dusty environments.
- Competitive Pricing for Bulk Orders: Provides discounts for large-volume orders, making it an ideal supplier for agricultural cooperatives, regional logistics hubs, and manufacturing plants requiring extensive pallet racking.
- Sturdy and Easy-to-Install Design: Pallet racks feature a simple, modular design that allows for quick and easy installation, reducing labor costs and project timelines.
- Adaptability to Harsh Environments: Products are treated with anti-corrosion coatings and can be customized for use in low-temperature environments (suitable for cold storage warehouses) and high-humidity regions.
- Strong Domestic Distribution: Has a network of distributors across 20 provinces in China, ensuring fast delivery of standard products and easy access to spare parts.
- Industry Experience with Agricultural Clients: With over 20 years of operation, Ruijing has deep understanding of the unique storage needs of the agricultural sector, providing tailored solutions that optimize space and improve inventory management.
10. Guangxi Guiqiang Storage Equipment Co., Ltd.
Guangxi Guiqiang Storage Equipment Co., Ltd. is a professional pallet racking manufacturer located in Nanning, Guangxi Zhuang Autonomous Region, established in 2004. The company specializes in the design, production, and installation of pallet racking systems, serving industries such as logistics, cross-border e-commerce, manufacturing, and retail. Guiqiang operates a 22,000-square-meter production facility, leveraging its strategic location in southern China near the ASEAN market to export products to Southeast Asian countries.
Guiqiang’s pallet racking product line includes selective pallet racks, drive-in racks, push-back racks, and cantilever racks, with a focus on cost-effectiveness and reliability. The company uses high-quality steel and advanced production technology to ensure product quality, with all products undergoing strict quality inspections before delivery. Guiqiang has established a strong presence in both domestic and international markets, exporting to Thailand, Malaysia, Indonesia, and Vietnam, and has become a preferred supplier for businesses looking to expand into the ASEAN region.
Characteristics and Advantages of Guangxi Guiqiang Storage Equipment Co., Ltd.
- ASEAN Market Expertise: Specializes in pallet racking solutions for businesses operating in the ASEAN region, with knowledge of local market needs, shipping routes, and regulatory requirements, providing seamless export services.
- Strategic Southern China Location: Located near major ports in Guangxi, reducing shipping costs and delivery times for exports to Southeast Asia, with international orders delivered within 10-20 days.
- Cost-Effective Standard Products: Offers high-quality pallet racking at competitive prices, making it a popular choice for small and medium-sized enterprises in China and Southeast Asia.
- Modular Design Flexibility: Pallet racks are designed with modular components that allow for easy expansion or reconfiguration as business needs change, providing long-term value for clients.
- Cross-Border E-Commerce Solutions: Develops pallet racking systems specifically for cross-border e-commerce warehouses, with high-density storage designs that accommodate large order volumes and frequent inventory turnover.
- Local After-Sales Support in ASEAN: Has established service partners in 5 Southeast Asian countries, providing on-site installation, maintenance, and spare parts support for international clients.
Conclusion
The pallet racking industry in China has evolved significantly over the past two decades, with suppliers combining advanced manufacturing technologies, innovative design, and customer-centric services to meet the diverse needs of global markets. The top 10 pallet racking suppliers in China for 2026, listed in this article, represent the best of the industry, from large-scale manufacturers with heavy industrial expertise to high-tech providers of smart storage solutions, and from specialized suppliers for specific industries to cost-effective options for small and medium-sized businesses. Each of these companies brings unique advantages, whether it’s advanced automation, customized design, strict quality control, or global service networks. As global logistics and manufacturing continue to grow, these suppliers are well-positioned to provide high-quality pallet racking solutions that help businesses optimize their storage operations, improve efficiency, and support supply chain growth. For businesses looking to invest in pallet racking systems in 2026 and beyond, partnering with one of these top suppliers ensures access to reliable, durable, and innovative storage solutions tailored to their specific needs.