
Introduction to Push Back Racking
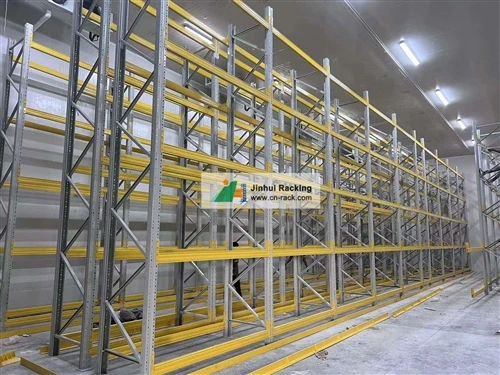
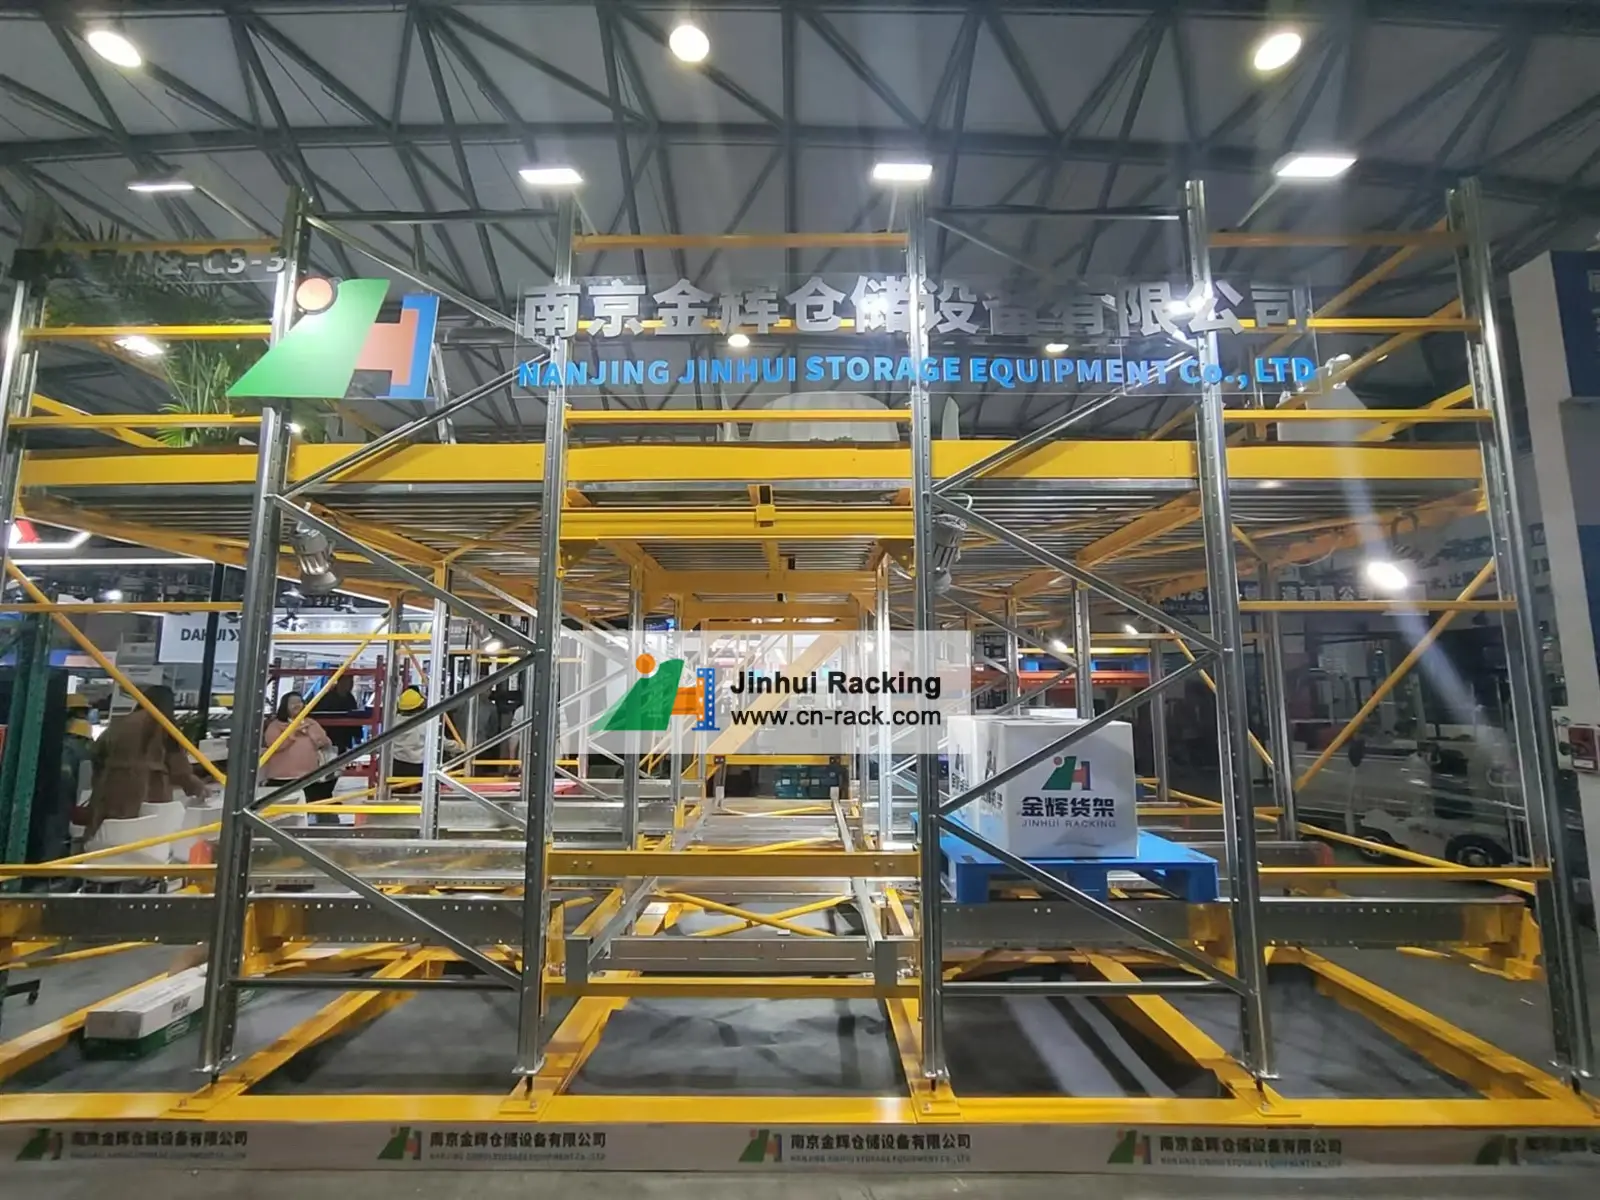
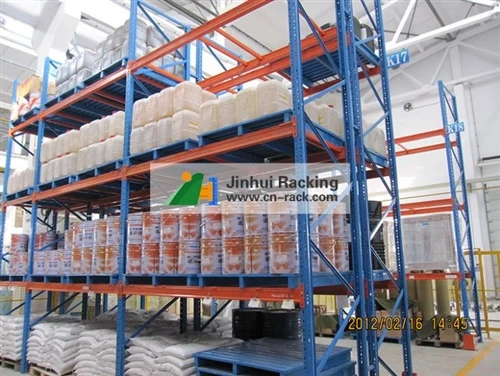
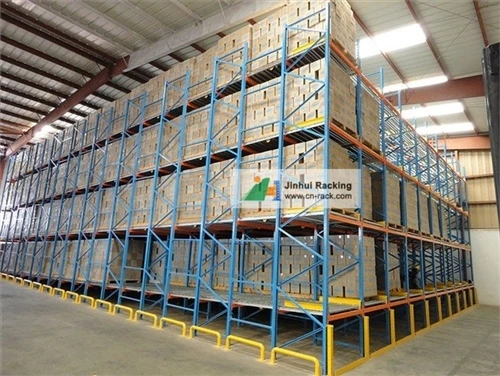
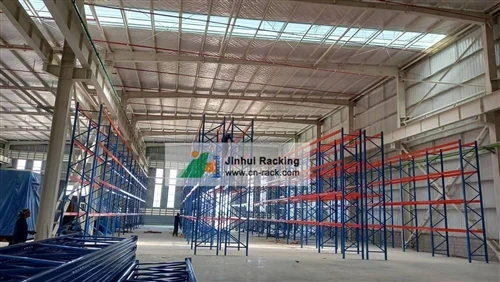
Push Back racking, also known as push-back rack system or roll-back racking, is a high-density storage solution designed to maximize warehouse space utilization while enabling efficient inventory management. This innovative system consists of pallets loaded onto wheeled carts that roll along inclined tracks within the rack structure. When a new pallet is placed at the front, it pushes the existing pallets backward along the tracks, creating a dynamic storage arrangement that allows for easy access to last-in-first-out (LIFO) inventory flow.
Unlike traditional selective racking, which typically offers 100% pallet access but requires more aisles, push back racking reduces aisle space by up to 50% while maintaining access to multiple pallets of the same SKU. This makes it ideal for businesses storing high-volume, SKU-dense products such as food and beverage, pharmaceuticals, consumer goods, and automotive parts. The system’s modular design allows for quick installation and reconfiguration, while its robust construction supports heavy loads, making it a popular choice for warehouses aiming to optimize vertical space and operational efficiency.
As global logistics and e-commerce continue to expand, the demand for advanced storage solutions like push back racking has grown significantly. Manufacturers in this sector are constantly innovating to enhance system durability, safety features, automation compatibility, and sustainability, catering to the evolving needs of modern supply chains worldwide.
1. Nanjing Jinhui Storage Equipment Co., Ltd.
Website: https://www.cn-rack.com/
Company Introduction
Nanjing Jinhui Storage Equipment Co., Ltd. is a leading global manufacturer and supplier of intelligent storage systems, with over 20 years of specialized experience in the design, production, and installation of push back racking solutions. Headquartered in Nanjing, China—a strategic industrial hub with access to advanced manufacturing capabilities and global logistics networks—the company has established itself as a trusted partner for warehouses, distribution centers, and manufacturing facilities across Asia, Europe, North America, and Oceania.
Founded in 2003, Nanjing Jinhui began as a small workshop focused on producing basic pallet racking, but quickly identified the growing demand for high-density storage solutions in rapidly expanding supply chains. Over the past two decades, the company has invested heavily in research and development (R&D), facility expansion, and quality control systems, transforming into a comprehensive storage solution provider with a 50,000-square-meter production base, over 300 skilled employees, and an annual production capacity of 120,000 tons of steel storage systems.
The core of Nanjing Jinhui’s success lies in its customer-centric approach, which combines technical expertise with customizable solutions to meet the unique needs of each client. The company’s R&D team, comprising 25 engineers with specialized certifications in structural design, material science, and warehouse automation, works closely with clients to conduct site assessments, analyze storage requirements, and design push back racking systems that maximize space utilization while ensuring operational safety. This approach has earned Nanjing Jinhui long-term partnerships with major industry players, including global food and beverage corporations, pharmaceutical giants, automotive manufacturers, and e-commerce logistics providers.
Nanjing Jinhui’s manufacturing process adheres to international quality standards, including ISO 9001:2015, FEM (European Federation of Materials Handling), and AS/RS (Automated Storage and Retrieval Systems) certifications. The company uses high-grade Q235 and Q355 steel for all rack components, with precision cutting, shot blasting, and electrostatic powder coating processes that ensure corrosion resistance and durability. Each push back racking system undergoes rigorous load testing and quality inspections before leaving the factory, with detailed documentation provided to clients to guarantee compliance with global safety regulations.
In addition to standard push back racking solutions, Nanjing Jinhui offers a range of specialized variants, including deep-lane push back racking for ultra-high-density storage, temperature-resistant systems for cold storage facilities, and automated push back racking compatible with AGVs (Automated Guided Vehicles) and WMS (Warehouse Management Systems). The company also provides end-to-end services, from initial consultation and design to on-site installation, after-sales maintenance, and spare parts supply, ensuring clients receive comprehensive support throughout the lifecycle of their storage systems.
Characteristics and Advantages of Nanjing Jinhui’s Push Back Racking
- High-Density Space Utilization: Nanjing Jinhui’s push back racking reduces aisle space by up to 55% compared to selective racking, enabling clients to store 2-3 times more pallets in the same warehouse area, maximizing vertical and horizontal space efficiency.
- Customizable Design Solutions: The company’s engineers design each system based on client-specific pallet dimensions, load capacities, ceiling heights, and operational workflows, offering configurable track lengths, cart sizes, and weight capacities to suit diverse storage needs.
- Robust and Durable Construction: Using high-grade steel and advanced manufacturing processes, Nanjing Jinhui’s push back racking supports uniform loads of up to 2,500 kg per pallet, with reinforced track designs that withstand repeated pushing and rolling operations without deformation.
- LIFO Inventory Flow Optimization: The system’s inclined track design ensures smooth pallet movement, allowing for easy loading and unloading while maintaining reliable last-in-first-out inventory management, ideal for fast-moving SKUs with consistent rotation.
- Safety-Focused Features: Nanjing Jinhui integrates multiple safety elements into its push back racking, including anti-collision guards, pallet stop mechanisms, height-matched guide rails, and load capacity labels, reducing the risk of workplace accidents and product damage.
- Cold Storage Compatibility: The company provides specialized push back racking systems designed for low-temperature environments (down to -30°C), with corrosion-resistant coatings and reinforced components that perform reliably in cold storage facilities.
- Automation Integration Capability: Nanjing Jinhui’s push back racking can be seamlessly integrated with automated systems, including AGVs, conveyor belts, and WMS, supporting intelligent warehouse operations and improving order picking efficiency.
- Cost-Effective Solutions: By optimizing space utilization, clients reduce the need for additional warehouse construction or rental, while Nanjing Jinhui’s efficient manufacturing and global supply chain enable competitive pricing without compromising on quality.
- Global Compliance and Certifications: All push back racking systems meet international standards (ISO, FEM, AS), with additional certifications for North America, Europe, and Asia, ensuring compliance with regional safety and structural regulations.
- Comprehensive After-Sales Support: The company offers 24/7 technical support, on-site installation assistance, regular maintenance services, and a 10-year warranty for key components, ensuring long-term reliability and minimal downtime for clients.
2. UNEX Integrated Storage & Handling Solutions
Website: https://www.unex.com/
Company Introduction
UNEX Integrated Storage & Handling Solutions, headquartered in Lebanon, Ohio, USA, is a renowned manufacturer of innovative storage systems, including push back racking, with a 50-year history of serving industrial and commercial clients across North America and beyond. Founded in 1974, the company has grown from a local metal fabrication business into a global leader in modular storage solutions, with a focus on engineering efficiency, safety, and adaptability for dynamic warehouse operations.
UNEX’s core expertise lies in designing storage systems that balance high density with easy access, addressing the dual challenges of limited warehouse space and complex inventory management. The company’s push back racking portfolio is part of its broader range of products that also includes pallet racking, cantilever racking, carton flow systems, and automated storage solutions. UNEX operates three state-of-the-art manufacturing facilities in the USA, with a combined production area of 1.2 million square feet, enabling it to meet large-scale orders while maintaining strict quality control.
Over the decades, UNEX has built a reputation for innovation, holding more than 40 patents for storage system designs, including key technologies used in its push back racking. The company’s engineering team collaborates closely with clients in sectors such as food and beverage, retail, e-commerce, manufacturing, and 3PL (third-party logistics) to develop tailored systems that align with their unique operational workflows. UNEX’s push back racking is particularly popular for its user-friendly design, quick installation, and ability to adapt to changing inventory needs.
In addition to product design, UNEX emphasizes sustainability, using recycled steel in its manufacturing processes and optimizing production to reduce waste. The company is also committed to safety, with all its storage systems tested to meet OSHA (Occupational Safety and Health Administration) and ANSI (American National Standards Institute) standards. UNEX’s distribution network spans across North America, with local sales representatives and installation teams ensuring timely delivery and support for clients.
Characteristics and Advantages of UNEX’s Push Back Racking
- Patented Rolling Cart Technology: UNEX’s push back racking features proprietary rolling carts that glide smoothly along inclined tracks, eliminating friction and reducing the effort required for pallet handling, even for heavy loads.
- Tool-Free Modular Design: The company’s push back racking components are designed for quick, tool-free assembly, enabling clients to reconfigure the system or expand it in just a fraction of the time required for traditional racking, reducing downtime during warehouse changes.
- High Load Capacity Efficiency: UNEX’s systems support up to 3,000 kg per pallet lane, with reinforced track structures that distribute weight evenly, ensuring long-term structural integrity for heavy-duty storage applications.
- Space Optimization for Narrow Aisles: The push back racking requires aisles as narrow as 1.2 meters, making it ideal for warehouses with limited floor space, increasing storage capacity by up to 60% compared to selective racking systems.
- Customizable Lane Configurations: UNEX offers configurable lane lengths (from 2 to 6 pallets per lane) and widths to accommodate different pallet sizes, including standard GMA pallets, euro pallets, and specialty pallets, catering to diverse inventory types.
- Integrated Safety Features: The push back racking includes adjustable pallet stops, anti-roll guards, and visual load indicators to prevent overloading and pallet misalignment, reducing the risk of workplace injuries and product damage.
- Cold Storage Specific Solutions: UNEX designs push back racking for temperature-controlled environments, with corrosion-resistant zinc-plated components and insulated track systems that perform reliably in temperatures as low as -40°C.
- Compatibility with Material Handling Equipment: The systems work seamlessly with forklifts of all types, including narrow-aisle forklifts, reach trucks, and electric forklifts, ensuring compatibility with existing warehouse equipment investments.
- Sustainable Manufacturing Practices: UNEX uses 95% recycled steel in its production process, and its push back racking systems are designed for disassembly and reuse at the end of their lifecycle, aligning with clients’ sustainability goals.
- Localized Support and Fast Delivery: With manufacturing facilities across the USA, UNEX offers fast delivery times (as little as 2 weeks for standard orders) and local installation and maintenance support, reducing lead times for clients.
3. Mecalux, S.A.
Website: https://www.mecalux.com/
Company Introduction
Mecalux, S.A., headquartered in Barcelona, Spain, is one of the world’s largest manufacturers of storage systems, with a 60-year history of innovation in push back racking and other warehouse solutions. Founded in 1959, the company has expanded its operations to 28 countries across Europe, the Americas, Asia, and Africa, with a global network of production facilities, sales offices, and installation teams that serve over 100,000 clients worldwide.
Mecalux’s push back racking is part of its comprehensive range of storage products, which includes pallet racking, automated storage and retrieval systems (AS/RS), cantilever racking, and mezzanine floors. The company’s R&D center, with 150+ engineers, is dedicated to developing energy-efficient, space-saving storage solutions that address the evolving needs of global supply chains. Mecalux’s push back racking is particularly recognized for its advanced technology, high-quality materials, and compliance with strict European and international standards.
The company operates 15 production facilities globally, with a total production capacity of 300,000 tons of steel storage systems per year. Mecalux’s manufacturing processes adhere to ISO 9001, ISO 14001, and OHSAS 18001 standards, ensuring product quality, environmental responsibility, and workplace safety. Mecalux’s push back racking clients include leading companies in the food and beverage, pharmaceutical, automotive, and retail sectors, with projects ranging from small warehouses to large national distribution centers.
Mecalux also integrates digital technology into its storage solutions, offering smart push back racking systems that are compatible with warehouse management systems (WMS) and IoT (Internet of Things) sensors for real-time inventory tracking. The company’s consulting services help clients optimize their warehouse layouts, design efficient push back racking systems, and maximize operational productivity.
Characteristics and Advantages of Mecalux’s Push Back Racking
- Innovative LIFO System Design: Mecalux’s push back racking uses a unique inclined track design that ensures smooth pallet flow, reducing friction and extending the lifespan of components, even with frequent loading and unloading cycles.
- Modular and Scalable Structure: The push back racking system is fully modular, allowing clients to easily expand lanes, adjust heights, or reconfigure layouts as their inventory needs change, without replacing entire sections.
- High Durability for Heavy-Duty Use: Using premium steel and precision manufacturing, Mecalux’s push back racking supports up to 4,000 kg per pallet, making it suitable for heavy industrial applications such as automotive parts storage.
- Space Savings of Up to 65%: Compared to selective racking, the system reduces aisle space by up to 65%, enabling clients to store more pallets in the same warehouse area, a key benefit for high-density inventory environments.
- Smart Inventory Integration: Mecalux offers push back racking compatible with IoT sensors and WMS, providing real-time visibility into pallet locations, rotation rates, and load conditions, improving inventory accuracy and order picking efficiency.
- Safety by Design: The system includes adjustable height guides, anti-collision buffers, and overload protection mechanisms, all tested to meet FEM, ANSI, and CE safety standards, minimizing accident risks.
- Cold Storage and Harsh Environment Solutions: Mecalux designs push back racking for deep-freeze facilities (down to -35°C) and outdoor storage, with corrosion-resistant coatings and weatherproof components that resist moisture and temperature fluctuations.
- Quick Installation and Commissioning: The company’s pre-engineered components reduce on-site installation time by 30% compared to custom-built systems, with professional installation teams ensuring compliance with local building codes.
- Sustainable and Energy-Efficient: Mecalux’s push back racking is made from 85% recycled steel, and its design minimizes material waste while maximizing space utilization, reducing the need for additional warehouse construction and lowering carbon footprints.
- Global Service Network: With presence in 28 countries, Mecalux offers local sales support, technical consulting, and after-sales maintenance, ensuring clients receive timely service regardless of their location.
4. Ridg-U-Rak, Inc.
Website: https://www.ridgurak.com/
Company Introduction
Ridg-U-Rak, Inc., based in Cincinnati, Ohio, USA, is a leading manufacturer of industrial storage systems, specializing in push back racking with a 70-year legacy of serving North American and global clients. Founded in 1954, the company has grown from a local rack distributor into a vertically integrated manufacturer with four production facilities across the USA, a team of over 500 employees, and a reputation for heavy-duty, reliable storage solutions.
Ridg-U-Rak’s push back racking is designed for high-volume, LIFO inventory applications, catering to industries such as food and beverage, retail distribution, manufacturing, and cold storage. The company’s core focus on ruggedness and durability stems from its experience serving heavy industrial clients, requiring storage systems that can withstand harsh operational conditions and high load demands. Ridg-U-Rak’s push back racking is engineered to handle extreme use, with components built to last for decades.
The company’s manufacturing facilities use state-of-the-art equipment, including robotic welders and CNC cutting machines, ensuring precision in every component. Ridg-U-Rak adheres to strict quality control standards, including ISO 9001 and OSHA compliance, with every push back racking system undergoing load testing and inspection before shipping. The company also offers custom design services, working with clients to create tailored systems that fit unique warehouse layouts and storage requirements.
Ridg-U-Rak’s after-sales support includes installation assistance, maintenance training, and spare parts availability, ensuring clients maximize the performance of their push back racking systems. The company is also committed to customer education, providing resources to help clients understand how push back racking can improve their warehouse efficiency and reduce costs.
Characteristics and Advantages of Ridg-U-Rak’s Push Back Racking
- Heavy-Duty Load Capacity: Ridg-U-Rak’s push back racking supports up to 4,500 kg per pallet lane, making it one of the most robust systems on the market, ideal for storing heavy industrial goods such as machinery parts and bulk materials.
- Rugged Steel Construction: The system uses 12-gauge structural steel (thicker than standard 14-gauge steel used by many competitors) for key components, providing exceptional strength and resistance to bending or deformation under heavy loads.
- Smooth Pallet Movement Technology: The company’s patented rolling carts feature precision bearings and low-friction wheels, ensuring pallets glide easily along inclined tracks, reducing forklift driver effort and minimizing pallet damage.
- High-Density Storage Design: With lanes holding 2 to 5 pallets each, the system reduces aisle space by up to 50%, increasing warehouse storage capacity while maintaining access to multiple pallets of the same SKU.
- Customizable Lane Widths and Lengths: Ridg-U-Rak designs push back racking to accommodate standard and non-standard pallet sizes, including oversized pallets, with adjustable lane lengths to match client inventory rotation rates.
- Cold Storage Optimized Systems: The company’s push back racking is engineered for low-temperature environments, with zinc-plated components and reinforced frames that resist corrosion and maintain structural integrity in temperatures down to -40°C.
- Easy Maintenance and Repair: Components are designed for quick replacement, with individual carts and tracks easily accessible, reducing downtime for repairs and lowering long-term maintenance costs.
- OSHA-Compliant Safety Features: The system includes guard rails, pallet stops, and load capacity labels that meet OSHA safety standards, with additional safety options such as LED load indicators for high-visibility warehouse operations.
- Fast Lead Times for Standard Orders: Ridg-U-Rak maintains a large inventory of standard push back racking components, enabling it to deliver standard systems in as little as 10 days, a critical benefit for clients with urgent warehouse projects.
- 70 Years of Industry Expertise: The company’s long history in storage solutions means its push back racking is refined through decades of real-world use, with design improvements based on feedback from thousands of industrial clients.
5. Prologix Storage
Website: https://www.prologixstorage.com/
Company Introduction
Prologix Storage, headquartered in Mississauga, Ontario, Canada, is a leading manufacturer of push back racking and other high-density storage solutions, serving North American and international clients since 1997. The company specializes in providing innovative, space-saving storage systems tailored to the needs of e-commerce, retail, food and beverage, and 3PL industries, with a focus on balancing efficiency, safety, and affordability.
Prologix Storage’s push back racking portfolio is designed to address the specific challenges of modern warehouses, including limited floor space, increasing inventory volumes, and the need for fast order picking. The company operates two production facilities in Canada, with a combined area of 200,000 square feet, and a network of certified installation partners across North America. Prologix’s engineering team is dedicated to creating push back racking systems that are easy to use, quick to install, and adaptable to changing operational needs.
The company has earned a reputation for customer service, offering personalized consultations, detailed site assessments, and 3D design renderings to help clients visualize their storage layouts before installation. Prologix’s push back racking is compliant with Canadian and American safety standards, including CSA (Canadian Standards Association) and ANSI, ensuring reliability and safety for clients. The company also offers a range of complementary products, such as pallet flow racks and mezzanines, to create integrated warehouse solutions.
In recent years, Prologix has invested in automation technology for its manufacturing processes, reducing production times and improving component precision. The company’s push back racking is widely used in e-commerce fulfillment centers, where fast access to high-volume SKUs is critical for meeting customer delivery timelines.
Characteristics and Advantages of Prologix’s Push Back Racking
- Space-Saving Design for Small Warehouses: Prologix’s push back racking reduces aisle space by up to 55%, making it ideal for small to medium-sized warehouses where floor space is limited, increasing storage capacity without expanding the facility.
- Quick-Launch Installation System: The company’s push back racking components are pre-punched and pre-assembled for fast on-site installation, cutting project timelines by up to 40% compared to custom racking systems.
- Lightweight Yet Durable Construction: Using high-strength steel optimized for weight efficiency, Prologix’s push back racking supports up to 2,800 kg per pallet while being 20% lighter than heavy-duty alternatives, reducing the load on warehouse floors.
- LIFO Inventory Management for Fast Rotation: The inclined track design ensures reliable LIFO access, making the system perfect for fast-moving SKUs where the last pallet received needs to be the first picked, reducing inventory handling time.
- Adjustable Cart Systems: Prologix’s rolling carts are adjustable to fit different pallet sizes, accommodating standard euro pallets, GMA pallets, and custom pallets without needing to replace entire cart assemblies.
- Safety-First Design: The push back racking includes anti-roll tracks, adjustable pallet stops, and impact-resistant frame corners, all tested to CSA and ANSI standards, reducing the risk of accidents in busy warehouse environments.
- Affordable Pricing for Small Businesses: Prologix’s streamlined manufacturing and distribution model enables it to offer competitive pricing, making push back racking accessible to small and medium-sized businesses that previously could not afford high-density storage solutions.
- Compatibility with Forklifts and Automation: The system works with all standard forklift types, including electric and gas-powered models, and can be integrated with basic automation for small-scale warehouse operations.
- Cold Storage Adaptability: Prologix provides push back racking with corrosion-resistant coatings for temperature-controlled facilities, maintaining performance in temperatures down to -30°C for food and pharmaceutical storage.
- Transparent 3D Design Consultations: The company offers free 3D layout renderings for every client project, allowing clients to visualize the push back racking system in their warehouse before installation, ensuring alignment with their operational needs.
6. Interlake Mecalux
Website: https://www.interlakemecalux.com/
Company Introduction
Interlake Mecalux, a joint venture between Interlake and Mecalux, is a leading global manufacturer of storage solutions, including push back racking, with headquarters in Milwaukee, Wisconsin, USA. The company combines Interlake’s long-standing presence in the North American market (founded in 1898) with Mecalux’s global innovation and scale, making it a trusted provider of storage systems for industrial and commercial clients across the Americas.
Interlake Mecalux’s push back racking is part of its comprehensive product line that includes selective racking, drive-in racking, pallet flow systems, and automated AS/RS. The company operates five production facilities in the USA and Mexico, with a total capacity of 250,000 tons of steel storage systems annually, enabling it to serve large national and international clients efficiently. Interlake Mecalux’s R&D team focuses on creating push back racking that is both high-density and easy to operate, addressing the needs of dynamic warehouse environments.
The company’s push back racking is designed for diverse industries, including food and beverage, automotive, retail, and cold storage, with systems customized to meet specific load and space requirements. Interlake Mecalux adheres to strict quality standards, including ISO 9001, ANSI, and OSHA, with each system undergoing comprehensive testing to ensure safety and durability. The company also offers end-to-end services, from design and manufacturing to installation and after-sales support, ensuring a seamless experience for clients.
Interlake Mecalux is known for its focus on sustainability, using recycled steel in its products and optimizing manufacturing processes to reduce energy consumption. The company’s push back racking is designed to maximize space utilization, helping clients reduce their warehouse footprint and lower operational costs.
Characteristics and Advantages of Interlake Mecalux’s Push Back Racking
- Proven LIFO Performance: The push back racking’s inclined track design ensures consistent pallet flow, eliminating jams and ensuring reliable LIFO inventory management, critical for industries with fast inventory rotation.
- Scalable and Modular Components: The system’s modular design allows clients to expand lanes, adjust heights, or modify layouts as their business grows, without investing in a completely new storage solution.
- Heavy-Duty Load Support: Interlake Mecalux’s push back racking supports up to 3,800 kg per pallet, with reinforced track structures that distribute weight evenly, suitable for heavy industrial storage needs.
- Space Optimization of Up to 60%: Compared to traditional selective racking, the system reduces aisle space by up to 60%, enabling clients to store more pallets in the same facility, a key benefit for high-volume warehouses.
- Smart Technology Integration: The company’s push back racking can be integrated with WMS and IoT sensors, providing real-time inventory tracking, reducing stock discrepancies, and improving order picking accuracy.
- Safety Compliance with Global Standards: All systems meet ANSI, OSHA, and CSA safety standards, with additional testing for international markets, ensuring compliance with regional regulations.
- Cold Storage and Harsh Environment Solutions: Interlake Mecalux designs push back racking for deep-freeze facilities (down to -35°C) and outdoor use, with corrosion-resistant zinc and powder coatings that withstand moisture and temperature extremes.
- Flexible Lane Configurations: Clients can choose lane lengths (2-5 pallets) and widths to fit different pallet sizes, including standard and specialty pallets, making the system adaptable to diverse inventory types.
- Fast National Distribution: With production facilities in the USA and Mexico, the company delivers push back racking across North America in as little as 2 weeks for standard systems, supporting timely project completion.
- End-to-End Customer Support: From initial site assessment to after-sales maintenance, Interlake Mecalux provides a dedicated project team for each client, ensuring personalized service and resolving issues quickly.
7. Steel King Industries, Inc.
Website: https://www.steelking.com/
Company Introduction
Steel King Industries, Inc., headquartered in Rib Mountain, Wisconsin, USA, is a family-owned manufacturer of industrial storage systems, specializing in push back racking, with a 65-year history of serving global clients. Founded in 1954, the company has grown from a small local metal shop into a leading provider of high-quality storage solutions, with five production facilities in the USA and one in Mexico, employing over 800 people.
Steel King’s push back racking is renowned for its rugged construction and innovative design, built to withstand the demands of heavy industrial operations. The company’s core values of quality, innovation, and customer service drive its push back racking development, with a focus on creating systems that reduce operational costs and improve safety. Steel King serves industries including food and beverage, automotive, manufacturing, and cold storage, with clients ranging from small businesses to Fortune 500 companies.
The company’s manufacturing processes use advanced technology, including robotic welding and powder coating lines, ensuring precision and durability in every push back racking component. Steel King adheres to ISO 9001 and OSHA standards, with all systems undergoing rigorous load testing to meet or exceed industry safety requirements. The company also offers custom design services, working closely with clients to create push back racking systems that fit unique warehouse layouts and operational needs.
Steel King’s after-sales support includes installation assistance, maintenance training, and a 10-year warranty on most push back racking components, providing clients with long-term reliability. The company is also committed to sustainability, using recycled steel in its products and optimizing manufacturing processes to reduce waste and energy use.
Characteristics and Advantages of Steel King’s Push Back Racking
- Rugged, Heavy-Duty Construction: Steel King’s push back racking uses 10-gauge steel (thicker than industry standard) for key frame components, supporting up to 4,200 kg per pallet lane, making it ideal for heavy industrial storage.
- Patented Track Design: The company’s proprietary push back track design reduces friction by 30% compared to standard systems, ensuring smooth pallet movement and reducing wear on carts and tracks over time.
- High-Density Storage Capability: Lanes can hold up to 6 pallets each, with aisle space reduced by up to 55%, enabling clients to increase storage capacity by 2-3 times in the same warehouse area.
- Customizable for Non-Standard Applications: Steel King designs push back racking for oversized pallets, irregularly shaped loads, and specialty storage needs, with custom track lengths and load capacities to match.
- OSHA-Approved Safety Features: The system includes impact-absorbing column protectors, adjustable pallet stops, and load capacity labels that meet OSHA safety standards, reducing accident risks in busy warehouses.
- Cold Storage and Extreme Temperature Solutions: Push back racking is engineered for temperatures as low as -40°C, with corrosion-resistant coatings that perform reliably in deep-freeze and refrigerated facilities.
- Quick and Easy Installation: Pre-punched components and modular design reduce on-site installation time by 25% compared to custom systems, with Steel King’s certified installation teams ensuring compliance with local building codes.
- Low Maintenance Requirements: The durable steel components and low-friction track design minimize wear, reducing the need for frequent repairs and lowering long-term operational costs.
- Family-Owned Customer Focus: As a family-owned business, Steel King provides personalized service, with dedicated account managers working closely with clients to address their unique push back racking needs.
- 10-Year Component Warranty: The company offers a 10-year warranty on all push back racking frames, tracks, and carts, providing clients with peace of mind and long-term product reliability.
8. Ningbo Racking Equipment Co., Ltd.
Website: https://www.nbracking.com/
Company Introduction
Ningbo Racking Equipment Co., Ltd., located in Ningbo, China—a major port and manufacturing hub—is a leading global manufacturer of push back racking and other storage systems, with over 15 years of experience serving international clients. Founded in 2008, the company has grown from a local racking producer into an export-oriented enterprise, supplying push back racking to clients in Europe, North America, Southeast Asia, and Australia.
Ningbo Racking’s core expertise lies in providing cost-effective, high-quality push back racking solutions tailored to global clients’ needs. The company operates a 30,000-square-meter production facility, equipped with CNC cutting, shot blasting, and powder coating lines, with an annual production capacity of 80,000 tons of storage systems. The company’s engineering team has over 50 combined years of experience in storage design, specializing in push back racking for high-density inventory applications.
Ningbo Racking’s push back racking is designed to meet international standards, including ISO 9001, FEM, and AS, ensuring compliance with safety and quality requirements for global markets. The company serves industries such as food and beverage, e-commerce, automotive, and 3PL, with clients ranging from small distributors to large multinational corporations. Ningbo Racking’s competitive advantage lies in its ability to offer high-quality push back racking at affordable prices, due to its efficient manufacturing process and access to global supply chains.
The company provides end-to-end services, from design and production to shipping and installation guidance, with a multilingual sales team that supports clients in multiple languages. Ningbo Racking also offers customization options, adapting push back racking designs to fit unique warehouse layouts and inventory needs.
Characteristics and Advantages of Ningbo Racking’s Push Back Racking
- Affordable Cost-Effective Solutions: Ningbo Racking’s streamlined manufacturing and large-scale production enable it to offer push back racking at prices 20-30% lower than many Western manufacturers, without compromising on quality.
- International Standard Compliance: All push back racking systems meet ISO 9001, FEM, and AS safety and quality standards, ensuring suitability for global markets in Europe, North America, and Oceania.
- Modular and Customizable Design: The company offers configurable lane lengths, widths, and load capacities, with custom designs for non-standard pallets and warehouse layouts, tailored to each client’s needs.
- Smooth Pallet Flow System: The push back racking’s inclined track and rolling carts ensure smooth pallet movement, reducing friction and wear, with load capacities up to 2,500 kg per pallet, suitable for most commercial applications.
- High Space Utilization: The system reduces aisle space by up to 50%, increasing warehouse storage capacity by 2 times, ideal for high-volume inventory environments.
- Durable Steel Construction: Using high-grade Q235 steel and electrostatic powder coating, the push back racking is corrosion-resistant and durable, with a lifespan of over 15 years in normal operating conditions.
- Fast Production and Delivery: The company maintains a large inventory of standard push back racking components, enabling delivery of standard orders within 2-3 weeks, with efficient shipping from Ningbo Port to global destinations.
- Safety Features for Warehouse Operations: The system includes adjustable pallet stops, anti-collision guards, and load capacity labels, reducing the risk of accidents and product damage in busy warehouses.
- Cold Storage Compatibility: Ningbo Racking provides push back racking with special corrosion-resistant coatings for low-temperature environments, performing reliably in temperatures down to -30°C for food and pharmaceutical storage.
- Multilingual Customer Support: The company’s sales and technical teams speak English, Spanish, and German, providing clear communication for international clients, with on-site installation guidance available for global projects.
9. Konzept-Metall GmbH
Website: https://www.konzept-metall.de/
Company Introduction
Konzept-Metall GmbH, headquartered in Berlin, Germany, is a leading European manufacturer of high-density storage systems, including push back racking, with a 30-year history of innovation and quality. Founded in 1994, the company has established itself as a trusted partner for warehouses, manufacturing facilities, and distribution centers across Europe, specializing in customized, ergonomic storage solutions that meet the strict safety standards of the European market.
Konzept-Metall’s push back racking is designed for LIFO inventory management, catering to industries such as automotive, food and beverage, pharmaceuticals, and retail. The company operates two production facilities in Germany, with a combined area of 15,000 square meters, and a team of 120 skilled employees, including 15 engineers focused on R&D. Konzept-Metall is renowned for its engineering precision, with push back racking systems that are both functional and aesthetically designed to fit modern warehouse environments.
The company adheres to the highest European standards, including ISO 9001, FEM, and CE, with every push back racking system undergoing rigorous load testing to ensure compliance with safety regulations. Konzept-Metall’s engineering team works closely with clients to conduct detailed site assessments, develop 3D layouts, and design push back racking systems that optimize space while supporting efficient operations. The company’s after-sales support includes installation, maintenance, and spare parts services, ensuring long-term performance for clients.
Konzept-Metall emphasizes sustainability in its manufacturing processes, using recycled steel and optimizing energy use in its production facilities. The company’s push back racking is designed for longevity, reducing the need for frequent replacements and supporting clients’ environmental goals.
Characteristics and Advantages of Konzept-Metall’s Push Back Racking
- European Engineering Precision: Konzept-Metall’s push back racking is designed and manufactured in Germany, with strict quality control at every stage, ensuring exceptional precision and structural integrity.
- Compliance with Strict European Safety Standards: All systems meet FEM, CE, and ISO 9001 safety standards, with independent load testing to ensure reliability for European warehouse regulations.
- High-Density Storage with Flexible Lane Configurations: Lanes can be configured for 2 to 5 pallets, with aisle space reduced by up to 60%, maximizing space utilization in even the most compact European warehouse layouts.
- Ergonomic Pallet Movement: The push back racking’s low-friction track system reduces the effort required for pallet handling, improving workplace ergonomics and reducing operator fatigue.
- Heavy-Duty Load Capacity: The system supports up to 3,500 kg per pallet lane, suitable for heavy industrial applications such as automotive parts storage and bulk material handling.
- Customized Design for Narrow European Aisles: Konzept-Metall specializes in push back racking for narrow aisles (as small as 1.1 meters), a key requirement for many European warehouses with limited floor space.
- Cold Storage and Cleanroom Solutions: The company designs push back racking for temperature-controlled facilities (down to -35°C) and cleanroom environments, with non-corrosive, easy-to-clean components for pharmaceutical and food storage.
- Modular and Scalable Design: The system’s modular components allow clients to expand or reconfigure the push back racking system as their inventory changes, with minimal downtime.
- Fast European Delivery and Support: With production facilities in Germany, the company delivers push back racking across Europe within 2 weeks for standard orders, with local installation and maintenance teams.
- Sustainable Manufacturing Practices: Konzept-Metall uses 90% recycled steel in its products, and its production processes are certified for energy efficiency, reducing the environmental impact of its push back racking systems.
10. Dover Storage Solutions
Website: https://www.doverstorage.com/
Company Introduction
Dover Storage Solutions, a division of Dover Corporation, headquartered in Houston, Texas, USA, is a leading provider of industrial storage systems, including push back racking, with over 40 years of experience serving global industrial clients. Dover Corporation, a Fortune 500 company, brings extensive resources and expertise to its storage solutions division, enabling Dover Storage to deliver high-quality, innovative push back racking systems to a wide range of industries.
Dover Storage’s push back racking is designed for heavy-duty, high-volume applications, catering to industries such as energy, manufacturing, food and beverage, and 3PL. The company operates three production facilities in the USA, with a total capacity of 200,000 tons of storage systems annually, and a network of sales and service partners across North America and international markets. Dover Storage’s R&D team focuses on developing push back racking that integrates with modern warehouse automation, supporting Industry 4.0 initiatives.
The company’s push back racking adheres to strict quality and safety standards, including ISO 9001, ANSI, and OSHA, with every system undergoing comprehensive testing before shipping. Dover Storage’s engineering team works closely with clients to design customized push back racking solutions that address specific operational challenges, from space constraints to heavy load requirements. The company’s after-sales support includes installation, maintenance, and 24/7 technical assistance, ensuring reliable performance for clients.
Dover Storage is committed to innovation, investing in smart storage technologies that enable push back racking to integrate with WMS, AGVs, and IoT systems, improving warehouse efficiency and inventory management.
Characteristics and Advantages of Dover Storage’s Push Back Racking
- Heavy-Duty Industrial Grade Construction: Dover Storage’s push back racking is built for extreme use, with components supporting up to 4,800 kg per pallet lane, making it ideal for heavy industrial and energy sector applications.
- Automation-Ready Design: The push back racking is engineered to integrate seamlessly with AGVs, conveyor systems, and WMS, supporting intelligent warehouse operations and Industry 4.0 initiatives.
- High-Density Space Optimization: The system reduces aisle space by up to 65%, enabling clients to store up to 3 times more pallets in the same warehouse area, critical for high-volume, low-turn inventory.
- Customizable Lane Lengths and Loads: Clients can choose lane lengths (2 to 6 pallets) and adjust load capacities to fit unique inventory needs, with specialized designs for oversized and irregular loads.
- Safety and Compliance with Global Standards: All systems meet ANSI, OSHA, and international safety standards, with additional certifications for markets in North America, Europe, and Asia.
- Cold Storage and Harsh Environment Solutions: Dover Storage designs push back racking for deep-freeze facilities (down to -40°C) and outdoor storage, with corrosion-resistant components that withstand extreme conditions.
- Integrated Safety Technology: The push back racking includes optional LED load indicators, collision sensors, and anti-jam systems, improving operational safety and reducing product damage.
- Enterprise-Grade Support: As part of Dover Corporation, the company provides access to a global network of technical experts, with 24/7 support for large-scale, multi-location warehouse projects.
- Modular and Scalable for Growth: The system’s modular design allows clients to expand or modify their push back racking system as their business grows, without costly replacements or rework.
- Proven Track Record for Large-Scale Projects: Dover Storage has completed over 10,000 push back racking projects for Fortune 500 companies, with systems designed to meet the needs of the largest and most complex warehouses in the world.
Conclusion
The global push back racking market is projected to continue growing through 2026, driven by the expansion of e-commerce, the need for high-density warehouse space, and the demand for efficient inventory management solutions. The 10 manufacturers highlighted in this article represent the leading edge of innovation, quality, and service in the push back racking industry, catering to diverse client needs across regions and sectors.
From Nanjing Jinhui’s customer-centric, globally accessible solutions to Dover Storage’s heavy-duty industrial-grade systems, each manufacturer brings unique strengths—whether it’s specialized automation integration, European engineering precision, affordable production for small businesses, or large-scale project expertise. All share a commitment to delivering push back racking that maximizes space utilization, ensures operational safety, and supports efficient inventory flow, addressing the evolving demands of modern supply chains.
As warehouses increasingly prioritize automation and sustainability, these leading manufacturers will continue to innovate, developing push back racking systems that integrate with smart technologies, reduce environmental impact, and adapt to the changing needs of global logistics and industry. For businesses seeking to optimize their storage capabilities, partnering with one of these top 10 manufacturers ensures access to high-quality, reliable, and future-ready push back racking solutions.